


 Chinese
 Spanish
 Russian
 Portuguese
 French
 German
 Indonesian
 Thai
 Vietnamese
 Arabic
 Italian
 Turkish
 Polish
 Japanese

Plastics silo monitoring should distinguish resin stock from material available at a machine, and both from the quantity of additive accepted into a recipe. Pellets, regrind and fine additives behave differently during storage and conveying. A METRAVON radar, point switch or weigh module should therefore be assigned a specific task, rather than expected to verify the complete material-handling process.
Follow the grade from delivery to the receiving hopper
Start with a drawing of silo identities, filling connections, conveying lines, diverter valves and destination hoppers. A correct level signal from the wrong silo is still the wrong production information. The control system needs an agreed relationship between each instrument tag, the material grade and the permitted route.
For facilities using virgin pellets and regrind, record their proportions and handling differences. Regrind can have a different particle shape and bulk density, so a volume-to-mass conversion established for one grade should not be carried into another without verification. A level sensor does not identify resin type, colour, moisture content or contamination.
Plastics silo monitoring with a solids radar
The MV-RD21S is an 80 GHz bulk-solids radar with a PE lens. It is a candidate for following the surface in an ambient-temperature resin silo, subject to the model's process limits and an installation review. A heated dryer hopper requires a separate temperature assessment, including the mounting connection and electronics environment.
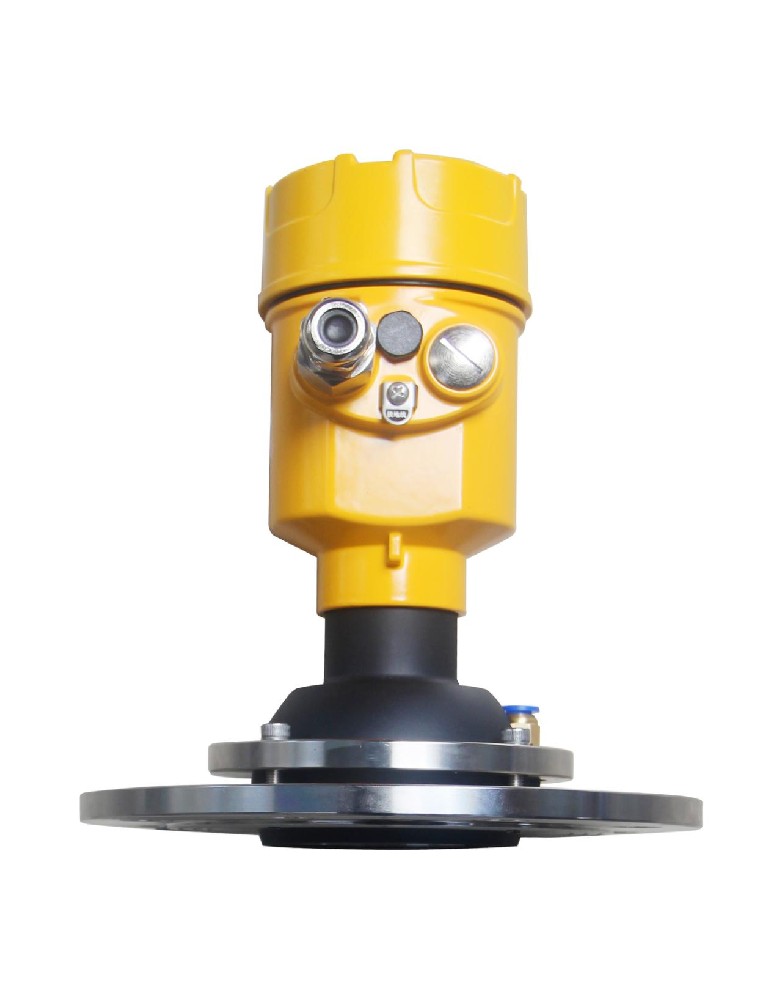
Pneumatic filling can produce a moving surface and fines near the inlet. Assess the path from the antenna towards the low-level surface, including ladders, braces and wall returns. Observe the reading during conveying and after settling. A clean empty-silo echo is useful evidence, but it does not demonstrate performance with the actual grade being delivered.
If the signal is used for purchasing stock, document the silo geometry and density assumptions. Compare the resulting estimate against receipts and consumption over a defined period. Keep a valid measured distance available for diagnosis; otherwise an incorrect density factor can be mistaken for a radar fault.
| Location | Reading | What remains unproven |
|---|---|---|
| Bulk silo | Surface trend and available storage estimate. | The grade identity and whether material is flowing through the outlet. |
| Receiver | Presence at a selected high or low point. | The mass transferred in the conveying cycle. |
| Dose hopper | Accepted change in weight for an ingredient addition. | Delivery to the mixer if material can remain in the downstream line. |
| Batch record | Recipe revision, requested quantity, actual quantity and exceptions. | Material identity unless the plant also controls the source and route. |
Treat a feed shortage as a flow problem before blaming inventory
A receiver can run empty while the main silo still contains substantial stock. Check conveying air, filter condition, diverter position, bridging and discharge equipment before recalibrating the silo radar. Compare the instrument trend with the conveying command and the receiving hopper's actual response.
A point detector such as MV-SP601 can provide a defined presence signal after the probe and material have been assessed. For a non-metallic or lined receiver, obtain the specified electrical reference arrangement. Do not assume the same mounting and sensitivity settings will transfer from an unlined metal bin.
Size additive weighing for the smallest meaningful dose
For small weigh hoppers, MV-WM0022 provides a bellows-module option. The module must carry the hopper and attached hardware as well as the ingredient. Its capacity is not a guarantee that a small colourant or additive dose will be resolved on a much larger gross load.
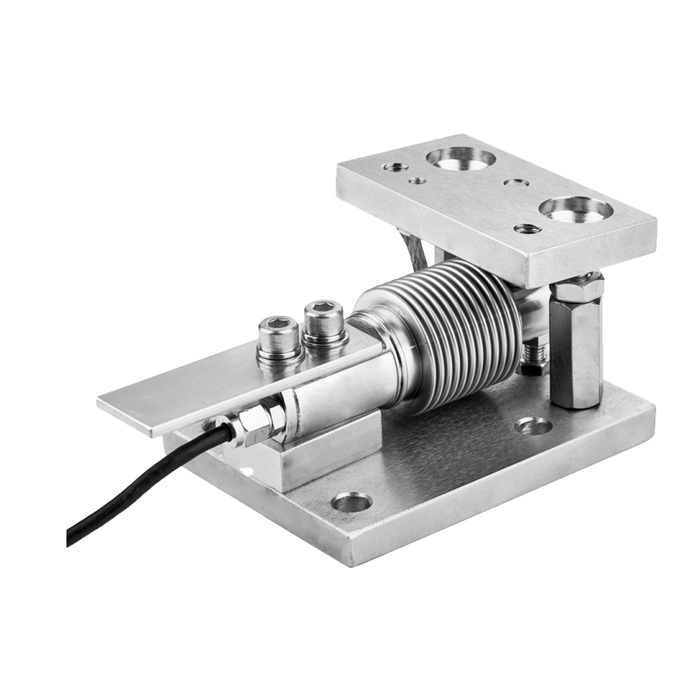
Compare weight before and after hose attachment, valve movement and pneumatic transfer. A stiff sleeve or pressure change can produce a force that looks like added material. Determine when the hopper is isolated, vented and settled enough for the quantity to be accepted. Test the smallest dose at the required production cycle, not only a static full-capacity load.
Where MV-WI0009 is proposed, state which functions belong to the instrument and which belong to the PLC. Recipe storage, grade permissions and rejected-batch handling must be specified; the availability of relay outputs does not establish those functions. Confirm the ordered serial or analogue option before designing the receiving interface.
Make changeover visible in the records
A new recipe number does not prove that the previous material has left the equipment. Identify likely retained-product locations, including receivers, feeders, discharge gates and transfer lines. Agree a clearance procedure and how the first material after changeover is handled. Record the old grade, new grade, affected route and release decision.
Retain failed transfers and interrupted additions rather than recording only completed cycles. On power restoration, a partially filled hopper should not automatically become a new empty starting point through tare. The restart sequence needs to resolve the material already present before another quantity is delivered.
Questions about resin storage and dosing
Q1. Can one density setting cover pellets and regrind?
Only if the required inventory accuracy is demonstrated for the relevant materials and mixtures. Otherwise keep material-specific conversion settings or report volume separately from estimated mass. For purchasing or production reconciliation, state the uncertainty introduced by the conversion.
Q2. Does a high silo level rule out a machine feed shortage?
No. Stock may be present above a bridge or outside the effective discharge channel, and the conveying system may be unable to transfer it. Diagnose the route using equipment states and receiving-hopper evidence instead of treating stored level as proof of flow.
Q3. Is a larger load-cell capacity always a safer choice?
It can increase mechanical capacity while reducing the useful signal from a small dose. Select against both the worst support load and the minimum required addition. Resolve impact and restraint problems in the mechanics rather than relying only on a larger rating.
Q4. What should a quotation request include?
Provide resin and additive types, silo and hopper drawings, conveying sequence, minimum dose, permitted error, changeover requirements and the PLC interface. Include the existing instrument tags so proposed replacements do not disturb grade-to-route identification.
Summary
Keep stock estimation, feed availability and dosing acceptance as separate decisions. Link them through reliable equipment identity and batch records. Request a METRAVON configuration for the identified measurement points, with the smallest additive quantity and actual conveying conditions included.
