


 Chinese
 Spanish
 Russian
 Portuguese
 French
 German
 Indonesian
 Thai
 Vietnamese
 Arabic
 Italian
 Turkish
 Polish
 Japanese

A batch weighing system has to deliver the required quantity after the feeder has stopped and the material has settled. A stable display during a bench test is not enough. The feeder, falling material, hopper connections, weight acquisition and control sequence all influence the accepted batch. METRAVON modules and weighing instruments should be selected against that complete cycle, including the smallest ingredient addition and the required production rate.
Define the batch result before selecting hardware
List the minimum and maximum additions for every ingredient, the permitted error for each addition, and the time available to complete the sequence. Decide whether the acceptance requirement applies to individual ingredients, total batch mass or both. Opposing ingredient errors can cancel in the total while leaving the recipe incorrect.
State whether the system weighs material gained by a receiving hopper or material lost from a supply vessel. A receiving hopper must settle before its final increase is accepted. A loss-in-weight arrangement must distinguish actual discharge from changes caused by refill, vibration or external forces. These approaches need different sequencing and test conditions.
A small additive weighed into a heavily loaded common hopper may produce only a small signal change relative to the gross load. More display decimals do not necessarily make that addition measurable. Compare a separate small weigh hopper with the common-hopper option if the required tolerance cannot be demonstrated across the full recipe.
Where batch weighing error enters the cycle
| Stage | Likely problem | Trial to include |
|---|---|---|
| Empty check | Residue or a hose force changes the starting weight. | Compare the starting condition after repeated discharges, without hiding the difference through automatic tare. |
| Coarse feed | Material impact and feeder vibration disturb the signal. | Record weight and feeder state during real material delivery, not only with static test weights. |
| Fine feed | Intermittent flow or bridging makes the delivery rate unpredictable. | Test the smallest addition and different supply-hopper levels with representative material. |
| Cutoff | Material already in transit continues entering the weigh hopper. | Compare the cutoff reading with the final settled result and the actuator stopping behaviour. |
| Settling | A long filter delay or premature stable decision accepts the wrong value. | Establish a stable-reading rule that meets the tolerance within the available cycle time. |
| Discharge | Retained material affects the next recipe or inventory record. | Check gate operation, residual weight and the response to an incomplete-empty condition. |
Cutoff compensation should be established from controlled trials with the actual feeder and material. It is not a universal value attached to a load-cell model. Flow can change with bulk density, moisture, supply head or feeder condition. Any automatic adjustment needs limits and an exception response so it does not continually compensate for a mechanical fault.
Match the hopper mechanics to the smallest addition
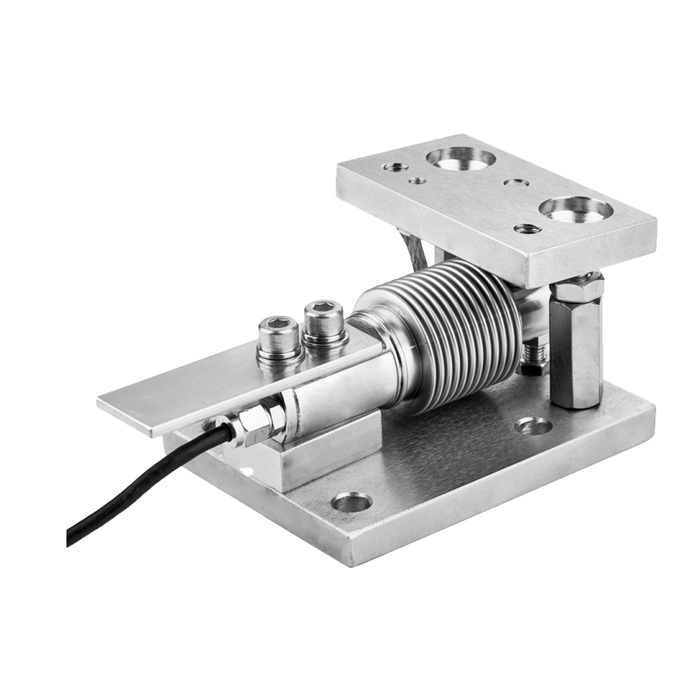
The MV-WM0022 uses a compact bellows assembly. Confirm the rated load of the complete module and its supplied load cell before selecting the support capacity. Include the hopper, gate, actuator and the worst load distribution, then check the electrical signal available from the minimum addition.
Flexible sleeves, extraction hoses and actuator lines should not support the hopper or pull it into a different position as a gate moves. Compare the indicated empty weight before and after each connection is installed. Test the final operating arrangement; a disconnected hopper can pass calibration and still perform poorly after the production hoses are reattached.
Keep material impact and transmitted vibration away from the weighing supports where the equipment design allows. The mechanical restraint and overload provisions must follow the selected assembly drawings. A module described for dynamic use does not, by itself, guarantee a particular dosing speed or final tolerance.
Assign control duties explicitly
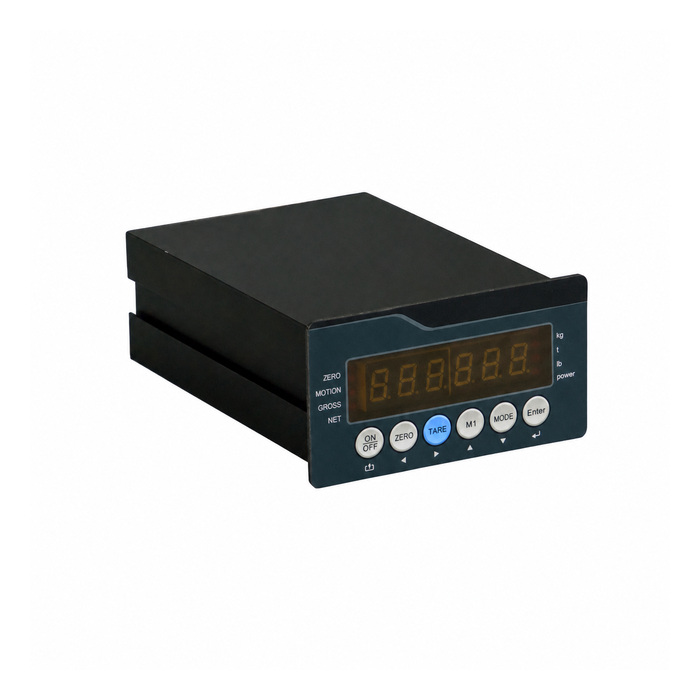
The MV-WI0009 is a candidate for weight indication and discrete I/O in a dosing installation. It lists four relay outputs, four isolated switch inputs and selectable RS232/RS485 communication. Modbus RTU and 4-20 mA are options to confirm in the order. These capabilities do not establish that every required multi-ingredient recipe function is built into the controller.
Write a sequence covering ready, start, coarse feed, fine feed, cutoff, stable acceptance, discharge and fault recovery. Map each required signal to an actual input or output. Confirm contact ratings and the need for intermediate switching devices; a relay-output count is not permission to switch a motor directly.
For PLC supervision, agree which device owns tare, recipe setpoints and final batch acceptance. Prevent conflicting commands from a local keypad and a remote program. Read the actual communication documentation for data type, units and status behaviour, and check any shared serial port when printing and PLC communication are both required.
Measure performance over representative batches
Test several operating conditions rather than presenting one favourable batch as acceptance. Include small and large recipes, low and high supply levels, normal feeder speed changes, and the materials most likely to bridge or continue flowing after cutoff. Use an independent reference appropriate to the permitted error.
Separate a consistent bias from variation between batches. Repeated overweight results suggest a different investigation from widely scattered results with the same average. Keep final error, settling time, total cycle time and rejected or interrupted cycles in the record. An average can hide individual batches outside tolerance.
Also test power interruption, lost weight data, a gate that does not confirm closed and a start command issued before the receiving equipment is ready. Agree whether a partial batch can resume, must be weighed again or requires operator disposition. Do not let a restart produce a normal completion record for an unverified quantity.
What a useful batch record contains
Retain the recipe revision, ingredient identity, requested quantity, accepted actual quantity, relevant tare, timestamps and batch status. Record adjustments and interrupted sequences instead of overwriting them. The weighing controller may provide signals, while recipe storage and reporting belong to the PLC or supervisory system; specify that division of scope.
When the objective is stock consumption as well as dosing, define where losses and retained product are accounted for. A recorded hopper discharge is not automatically equal to the quantity reaching a mixer if the transfer path can retain material. The inventory measurement guide explains why operational stock estimates and accepted batch quantities should remain distinguishable.
Batch-control questions
Q1. Can stronger filtering cure overshoot?
It can make a fluctuating display steadier, but added delay can make a cutoff occur later. First determine whether the error comes from signal disturbance, actuator delay or material still falling. Evaluate filtering together with the feed sequence and final settled mass.
Q2. Why do small doses fail when the large batch passes?
The permitted absolute error may be much smaller for the minor ingredient, while hopper tare and mechanical disturbances remain. Check signal utilisation, minimum stable addition and feeder repeatability. A separate small-capacity weighing stage may be more suitable than changing only the display resolution.
Q3. Can existing load cells be retained with a new controller?
Compare sensitivity, excitation, bridge resistance, wiring and the combined sensor load with the new input specification. Retaining the sensors does not remove the need to recalibrate and repeat the dosing trials, especially if filtering or command timing changes.
Q4. What should be sent for an equipment quotation?
Send the recipe range and tolerances, hopper drawing and tare, feeder type, required cycle time, control sequence and PLC details. Identify the electrical supply, existing sensors and required reporting functions. Ask for the proposed hardware and software responsibilities to be listed separately.
Summary
Judge batch weighing by the accepted material quantity and cycle performance, not display appearance. Match support capacity, feeder behaviour and control timing, then prove the result with representative trials. Request a METRAVON dosing configuration review with the smallest addition, allowed error and complete sequence.
