


 Chinese
 Spanish
 Russian
 Portuguese
 French
 German
 Indonesian
 Thai
 Vietnamese
 Arabic
 Italian
 Turkish
 Polish
 Japanese


A battery assembly force sensor should be selected around the operation being judged, not a general label such as battery pressing. Seating a component, compressing a module and holding a fixture can require different force intervals and different evidence of an acceptable cycle. Define the approved process requirement first, then specify how force will be measured and associated with position and time.
Define the decision made from the force trace
Identify the exact operation and the product variant. State whether acceptance depends on force at a specified position, a peak within a travel interval, a holding force or another validated feature. A maximum-force value alone may not distinguish correct seating from a part that jams earlier in the stroke.
Obtain operating limits from the approved product and process specifications. Sensor capacity is not an allowable compression force for a cell or module. No universal pressure, force, dwell time or reject threshold follows from the sensor model number.
Where pressure is the process quantity, define the loaded area and contact distribution. Dividing total force by nominal area gives an average under the stated assumptions; it does not establish uniform pressure across a flexible or uneven stack. A single force sensor cannot independently reveal every local pressure concentration.
Battery assembly force sensor placement determines what is measured
Draw the actuator, tooling, guides, product, supports and reaction frame. Mark the force path through the proposed sensor and any alternate paths through stops, guide friction or adjacent hardware. A transducer upstream of substantial guide friction may indicate actuator effort rather than the product contact force required by the acceptance rule.
Check platen stiffness and parallelism where several contact points share load. Total force does not prove equal distribution among parts. If uneven loading is a quality concern, identify the additional inspection or measurement needed instead of attributing that capability to one compression channel.
Include tooling weight and preload in capacity selection. Assess the maximum actuator capability, a misplaced part and a blocked stroke in the machine design. Protective stops and drive limits must be engineered for those conditions without carrying an uncontrolled share of normal measuring force.
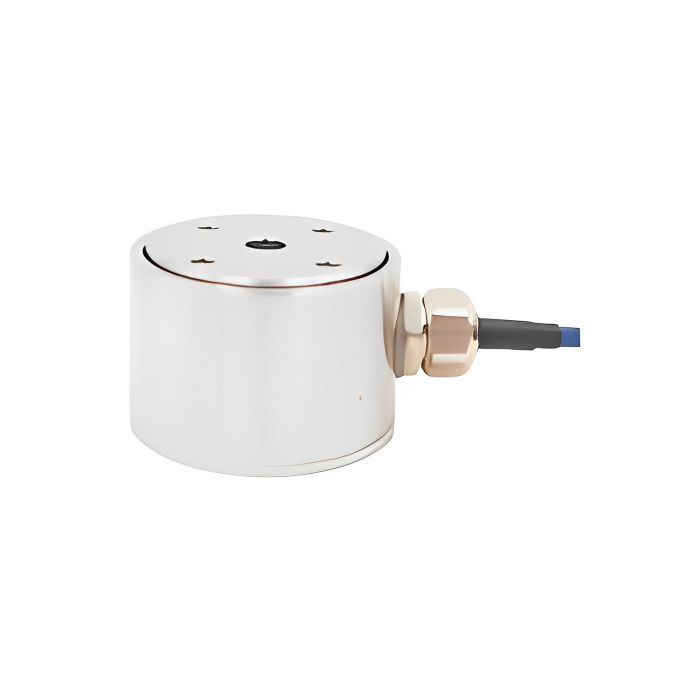
Use MV-LC0172 within its documented scope
| MV-LC0172 item | Reference | Decision for the assembly station |
|---|---|---|
| Force direction | Compression | Use a different approved arrangement if tensile force during withdrawal is part of the acceptance requirement. |
| Listed capacities | 100 / 200 / 500 N; 1 / 2 / 5 / 10 kN | Select the exact range from the validated process interval and mechanical load assessment. |
| Nominal sensitivity | 1 mV/V | Check signal size and noise at the force changes used for pass/fail decisions. |
| Reference excitation | 5 V | Specify compatible bridge conditioning and the final data interface. |
The METRAVON MV-LC0172 is a compact stainless-steel compression design. Its catalogue does not establish battery-process qualification, chemical compatibility with electrolyte, an electrostatic-control classification or performance for a particular production cycle. Confirm the actual exposure and machine requirements rather than inferring them from enclosure or material descriptions.
Request the drawing before finalising the sensor pocket and loading faces. Allow cable strain relief and service access without using a guard or cover as another force path. The compact force-fixture guide explains the difference between fitting a sensor physically and resolving a useful force signal.
Synchronise force, displacement and the recipe
Define where displacement is measured. Actuator travel can include movement from frame, tooling and sensor compliance; it is not necessarily the deformation of the product. If the acceptance rule refers to product compression or seating travel, establish the appropriate reference and any corrections.
Force and position samples must describe the same part of the cycle. Record the acquisition timing and filtering on both channels. Different delays can shift the apparent force-position relationship even when the raw measurements are individually correct. Choose timing requirements from the fastest event that affects acceptance, not from a generic sampling-rate recommendation.
Keep the recipe revision, product variant, fixture identification and measurement validity with the cycle result. A missing, saturated or stale force channel must not silently become a pass. Verify how the controller and production record distinguish an invalid measurement from a valid value outside the process window.
Qualify the measurement before adjusting reject limits
Check the force chain against an appropriate reference with the final tooling configuration. Retain initial readings, calibration changes and repeated results. Verify the displacement reference separately, then assess the combined trace under the approved process-validation plan.
Use qualified sample parts or approved fixtures to test acceptance and rejection logic without creating unsafe cell conditions. Include the permitted variations in tooling, recipe and operating state. A force calibration alone cannot prove that a pass/fail window distinguishes acceptable product.
If a holding-force trace drifts, compare the measurement baseline and machine temperature before changing limits. Investigate tooling movement, thermal expansion and actual product relaxation as separate possible causes. Raising a threshold to recover production yield can hide the change that the measurement was installed to detect.
For an enquiry, provide the operation, approved force interval, fixture drawing, displacement reference, cycle timing and required decision features. Add environment, conditioner and controller details through the METRAVON contact page. Separate the sensor and electronics scope from process qualification and machine commissioning.
Questions about production acceptance
Q1. Can peak force alone confirm that a part seated correctly?
Only if the qualified process shows that peak force is sufficient for that decision. A jam or early contact may produce a similar peak at a different position. Use the validated force-position or time criteria required for the operation, rather than adding or removing features simply to simplify the software.
Q2. What needs rechecking after the pressing tool is replaced?
Review alignment, contact geometry, preload and the displacement reference, then verify the affected measurement and process checks. A nominally identical tool can still change the force path or trace. Keep the tool revision and test results with the production configuration.
Summary
Choose the sensor from a defined battery assembly operation and approved process limits. Verify what reaches the sensing element, synchronise force with the correct position reference and test the decision logic independently of calibration. MV-LC0172 can be assessed as a compression component; the process evidence must establish whether the completed station makes a reliable quality decision.
