


 Chinese
 Spanish
 Russian
 Portuguese
 French
 German
 Indonesian
 Thai
 Vietnamese
 Arabic
 Italian
 Turkish
 Polish
 Japanese


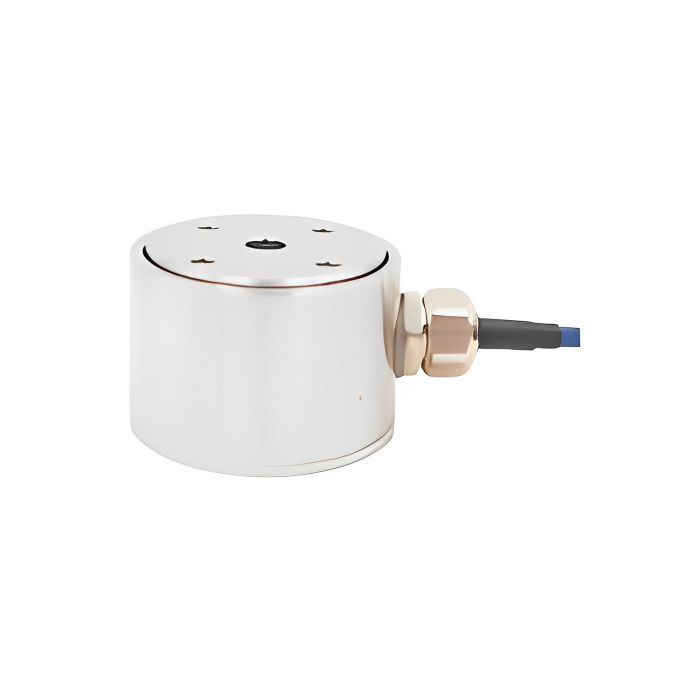
Miniature force sensor selection involves two different limits: available installation space and the smallest force that must be distinguished. A compact body does not necessarily have a low measuring range. For a press tool, assembly fixture or contact-force test, specify the useful force interval before choosing the smallest sensor that fits the drawing.
Miniature force sensor selection: compact is not the same as low-force
The METRAVON MV-LC0172 lists 100, 200 and 500 N, plus 1, 2, 5 and 10 kN capacities. Its reference data identify a stainless-steel compression design. If a process needs a force range below the smallest listed capacity, request a review of that requirement instead of treating the word miniature as evidence of adequate low-end performance.
State the smallest acceptable force difference separately from maximum force. A machine may need to reject a part because of a small change during contact while also surviving a much larger insertion force. That difference determines the required signal quality and test method; selecting only from the highest force can leave the decision signal too small.
| MV-LC0172 item | Reference value | What to check in the fixture |
|---|---|---|
| Nominal sensitivity | 1 mV/V | Specify the bridge amplifier range and verify the smallest useful signal. |
| Reference excitation | 5 V | Use the offered configuration's electrical requirements; a PLC voltage input is not a bridge supply. |
| Input resistance | 350 +/-30 ohm | Check excitation loading and the wiring arrangement. |
| Output resistance | 350 +/-3 ohm | Keep signal and excitation specifications separate when comparing electronics. |
| Non-linearity | ±0.1% of nominal force Cn | This is a force-based specification, not resolution or the complete installed measurement error. |
At nominal 1 mV/V and 5 V excitation, full-scale signal change is 5 mV. The specified ±10% sensitivity tolerance gives 4.5-5.5 mV at rated force before individual calibration. On a 100 N version, an ideal 1 N increment corresponds to 50 microvolts. This calculation describes signal size, not guaranteed detectability. The amplifier, wiring, mechanical repeatability and noise determine whether that increment can be used reliably.
Draw the contact and the support, not just the pocket
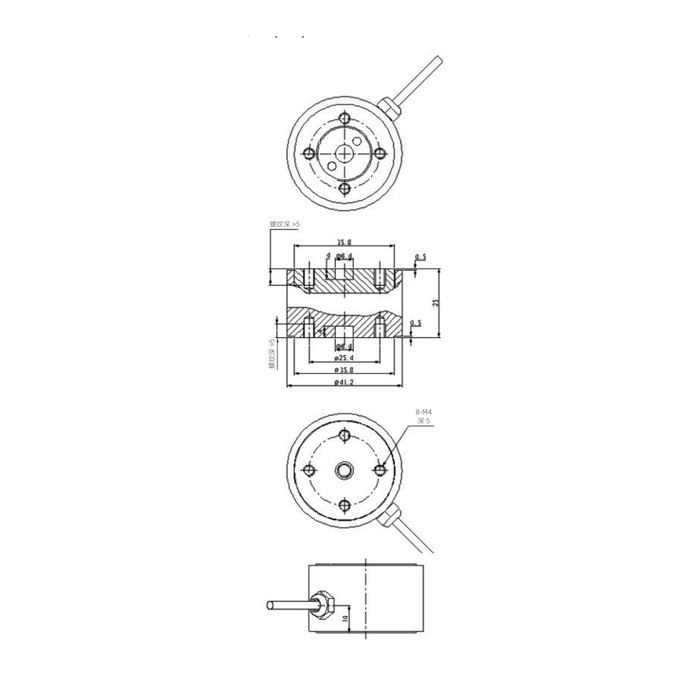
A small recess can leave too little room for correct force introduction. Identify the intended loading surface, support surface and fixing features from the capacity-specific drawing. Check the mating parts' stiffness and alignment. Do not transfer force through the cable outlet or an incidental part of the housing.
A probe contacting away from the intended axis can add bending. Guides may be necessary to control tooling movement, but friction in a guide can also divert force from the sensor. Test the assembled tool through its actual travel to establish whether the reading represents contact force or includes variable guide resistance.
Allow access for mounting and removal. An installation that traps the cable under a cover or requires pulling on it during service can create a repeatable source of damage. Locate the termination and strain relief so the cable does not push on the measured tooling.
Separate useful force from a machine jam
List the force during approach, normal contact, full stroke and release. Then assess faults such as a misplaced part or a blocked actuator. An overload allowance in the sensor data is not a reason to let the drive use the sensor as a mechanical stop.
Specify any protective stop or bypass through an approved mechanical design. It must not carry an unknown part of the normal measuring load. Its required clearance depends on the complete assembly movement and the sensor's permitted deformation; no universal gap can be assigned from the rated capacity alone.
For repeated loading, obtain the relevant duty information. A static capacity table does not state fatigue life, resonant frequency or a usable sampling rate for the installed fixture. Include the force-time profile when requesting confirmation for a rapid cycle.
Test the force at the time the machine uses it
Compare a suitable reference with the assembled tooling at the operating positions. Retain increasing and decreasing readings and repeated cycles before changing calibration. Run the machine in a controlled condition with no intended process contact to see whether motion itself produces a signal from cable movement or guide friction.
Where a short peak determines acceptance, inspect the recorded waveform and the controller value together. Filtering can make a trace look quiet while reducing or delaying the event of interest. Neither the PLC scan rate nor the number of displayed digits proves the complete measurement is fast or quiet enough.
For a quotation, send METRAVON the available envelope, tooling drawing, force interval, smallest decision increment, cycle timing and environment. Include the amplifier or PLC input specification. The custom-machine guide explains how to agree the station test, and the enquiry page provides a route for reviewing the proposed configuration.
Questions about restricted-space fixtures
Q1. Can the compression sensor measure pull force through an attached bracket?
Do not infer tensile capability from mounting holes or from an adapter that can be attached. Use a sensor explicitly intended for tension and confirm the complete attachment. A bracket cannot give a compression-only sensing arrangement an undocumented tensile rating.
Q2. Should capacity be increased just to protect against operator handling?
First assess how handling force reaches the sensor and whether guarding or an approved stop can prevent it. A higher capacity may reduce useful signal for the actual test. Choose capacity and handling protection together rather than sacrificing measurement performance without addressing the cause.
Summary
For a compact fixture, approve both the force interval and the mechanical envelope. MV-LC0172 provides documented compression configurations, but low-force resolution and rapid-cycle performance still require a system-level test. A dimensioned fixture and a clear acceptance threshold make the enquiry far more useful than a request for the smallest available sensor.
