


 Chinese
 Spanish
 Russian
 Portuguese
 French
 German
 Indonesian
 Thai
 Vietnamese
 Arabic
 Italian
 Turkish
 Polish
 Japanese


Load cell selection for custom machines should begin with the measurement station, not the space left inside the frame. A press fixture may need axial force at a particular point in its stroke; a weighing station may need the settled mass of a container. Those tasks can require different mounting arrangements, capacities and instrument behaviour even when both send a value to the same PLC.
Load cell selection for custom machines starts with the cycle
Describe one complete operating cycle and mark when the measurement is used. Include loading, approach, contact, measurement, release and return. State whether the controller needs a settled value, an average over part of the cycle or a short peak. A sensor that reads correctly while the machine is stationary has not demonstrated that it captures the required event during motion.
Record the minimum and maximum useful force, fixture preload and credible abnormal loads. A jam, actuator overshoot or operator pressing on a fixture can load the sensor outside the normal production cycle. Define those conditions before selecting capacity or overload protection. Taring away a fixture weight does not remove it from the mechanical load.
Also define the consequence of a missing or implausible measurement. Monitoring quality and providing a protective machine function are different requirements. Do not assign a safety role to an ordinary sensor solely because its measuring range exceeds the expected force; the complete protective design needs its own assessment.
Choose the arrangement that measures the intended quantity
| Machine station | METRAVON candidate | Condition to resolve first |
|---|---|---|
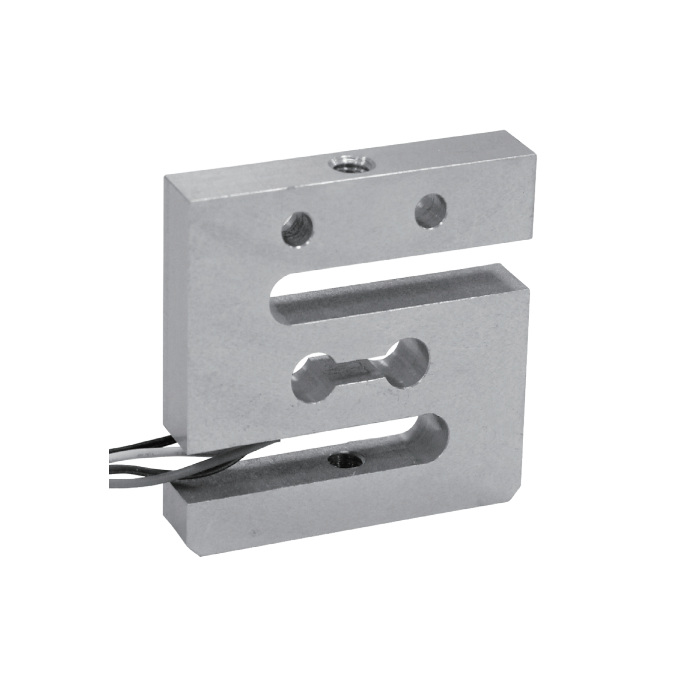
| Low-force pull or push fixture | MV-LC0190 tension and compression load cell | The attachments must transmit the required axial force without an uncontrolled bending load. |
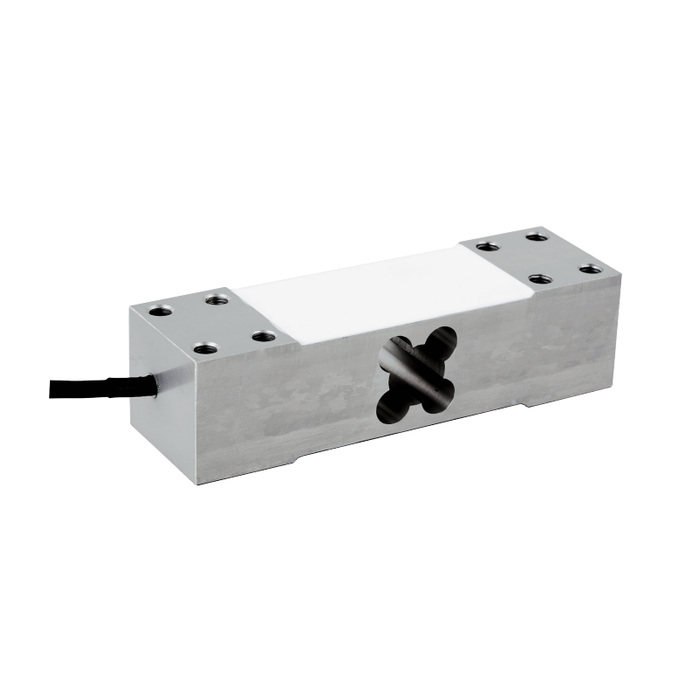
| Compact container-weighing platform | MV-LC0211 single-point load cell | The complete deck, capacity and off-centre loading arrangement need approval for the selected version. |
The MV-LC0190 lists 1, 5, 20 and 50 kg rated loads. The MV-LC0211 lists capacities from 50 to 500 kg for a different mechanical task. A similar outside envelope or overlapping capacity does not make the two arrangements interchangeable.
Draw the reaction path as well as the force entry point. A guide, bearing, stop or adjacent part can carry force around the sensor. In an axial fixture, misaligned attachments can add moment; in a weighing station, a conveyor transfer or hose can preload the platform. Identify what touches the measured assembly in each machine state.
Release the mechanical and electrical drawings together
The mechanical drawing should identify mounting faces, fasteners, intended force direction, clearance through the cycle and access for removal. Obtain the capacity-specific sensor drawing before machining the fixture. If sensor deflection or fixture compliance affects the process, request the relevant data rather than assuming the sensing element is perfectly rigid.
Keep overload stops separate from normal measurement contacts. Their design needs the permitted movement and load conditions, not an arbitrary gap copied from another machine. A stop that touches during measurement can bypass part of the load; a stop that acts too late provides no useful protection.
The electrical drawing should identify the bridge excitation and input, the sensor cable termination and the final interface. For MV-LC0190, the 1 kg version has a different nominal mV/V sensitivity from the higher capacities. Preserve that distinction in the instrument configuration and replacement documentation.
Test timing at the decision point
A fast PLC scan does not establish the response of the complete measurement chain. The amplifier, conversion, filters and communication can delay a result before the controller reads it. Request the applicable response information and test the signal at the point where the machine accepts, rejects or stops the process.
Do not infer bandwidth or fatigue life from a static capacity rating. The product data used here do not establish a complete dynamic performance limit for either installed station. For a rapid or repeated-force application, provide the expected force-time profile and cycle conditions for review.
The raw sensor output is not itself 4-20 mA or Modbus RTU. Specify the instrument that provides the required controller interface and verify its fault indication as well as its normal scaling. The PLC signal-chain guide covers that connection without assuming a universal register map.
Use the prototype test to close the specification
Apply reference loads through the assembled fixture or platform and compare repeated cycles under the intended operating conditions. Include loading and unloading, zero return, relevant positions and the final controller value. Retain the readings before calibration changes so the test can distinguish a mechanical problem from an instrument adjustment.
For an enquiry, send METRAVON the station drawing, cycle description, force range, smallest required change, environment and available bridge input through the contact page. Identify which dimensions are fixed and which can still change. This allows the sensor and instrument to be assessed before the machine design makes a different arrangement expensive.
Questions during machine development
Q1. Can automatic zeroing compensate for a changing fixture load?
Only zero under a verified reference condition. An automatic zero applied while a part remains in contact can hide a real process force or a jam. Define the permitted machine state, adjustment limits and diagnostic response, then test those conditions rather than enabling zero tracking as a general cure for drift.
Q2. Can the prototype calibration be copied to every production machine?
It can inform the procedure, but it does not verify each assembled machine. Fixture tolerances, sensor sensitivity and electronics can differ. Establish a production acceptance test and keep the results and settings with each machine, even when the bill of materials is identical.
Summary
Select the sensor around the quantity and moment the machine must measure. Approve the fixture, signal chain and acceptance test together. The model number then belongs to a defined measurement station, rather than becoming a component that the controls team must make usable after assembly.
