


 Chinese
 Spanish
 Russian
 Portuguese
 French
 German
 Indonesian
 Thai
 Vietnamese
 Arabic
 Italian
 Turkish
 Polish
 Japanese


An 80 GHz tank radar acceptance test should show what the installed instrument can measure, not simply that its display turns on. A steady reading in an empty vessel leaves several questions unanswered: will it follow the liquid during filling, recover after foam subsides, and report a measurement fault correctly? Agree the evidence needed for acceptance before commissioning starts, while access, reference measurements and representative operating conditions can still be arranged.
Build the 80 GHz tank radar acceptance test around the operating cycle
List the conditions that change the measurement: minimum and maximum operating levels, filling, withdrawal, agitation, temperature changes and any cleaning cycle. Select the relevant states for this tank rather than copying a standard list into every project. A quiet storage tank and a mixing vessel need different demonstrations even if they use the same radar family.
For each state, record the reference method, expected indication, allowable difference and response requirement. The allowable error should come from the measurement duty and agreed instrument specification. It should not be chosen after seeing the test results. If the reference method cannot resolve the required tolerance, improve the test arrangement or qualify the conclusion.
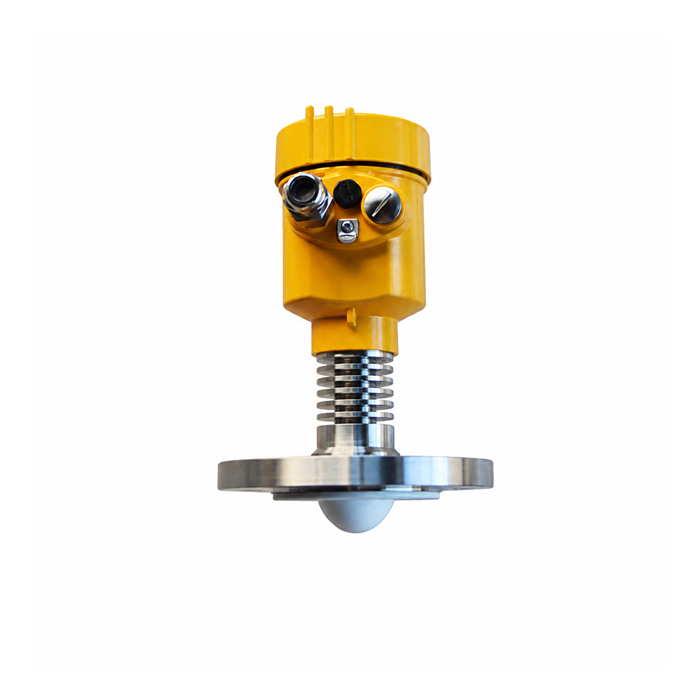
The METRAVON MV-RD14 is a liquid-level radar with a 44 mm lens antenna. Its family name identifies a candidate, not a completed site acceptance. Attach the offered configuration, process connection, antenna arrangement and installation drawing to the test record so the result applies to an identifiable assembly.
Establish a reference before comparing numbers
Radar distance, vessel level and the reference instrument must refer to compatible datums. A level measured upward from the tank floor cannot be compared directly with a distance measured downward from the antenna. Document the conversion and verify the installed reference point, including any adapter that changes the antenna position.
Take paired readings at the same time, or account for the level movement between observations. For an illustrative check, a reference level of 2.500 m and an indicated level of 2.496 m give a signed difference of -4 mm. That arithmetic alone does not establish a pass: the reference uncertainty, surface movement and agreed tolerance still matter. These numbers are a calculation example, not an MV-RD14 accuracy claim.
A delivery ticket or nominal tank capacity is not automatically a level reference. Volume can change with temperature, vessel geometry may be uncertain, and some liquid may remain in connecting pipework. For tests involving inventory conversion, use the separate level-to-inventory checking procedure; do not attribute every volume discrepancy to the radar.
| Test state | Evidence to retain | Decision |
|---|---|---|
| Steady level | Paired reference and indicated values, common datum and observation time. | Assess agreement against the defined tolerance and reference quality. |
| Filling | Level trend, filling state and any interrupted or invalid readings. | Confirm tracking and response throughout the tested rate and level interval. |
| Disturbance | Actual foam, mixing or temperature condition and available diagnostic records. | Identify whether the reading remains usable or enters the required fault state. |
| Recovery | Time and conditions under which a valid measurement returns. | Check automatic recovery without an unexplained reset or parameter change. |
Keep measurement tests separate from signal simulations
Injecting a current into a PLC input can verify input scaling and some downstream logic. It does not test the antenna, echo selection or installed radar. Likewise, a transmitter's output-simulation function bypasses part of the measurement chain. Label the starting point of each test so an electrical check is not mistaken for a successful level test.
Where available, save the echo or diagnostic record alongside the reference level and operating state. A screenshot without a time, tank tag or level reference is difficult to interpret later. A strong return is not sufficient if the instrument is following a nozzle or internal structure instead of the surface.
Test the configured invalid-measurement behaviour under an approved commissioning procedure. Confirm what the local instrument, receiving input and operator display each show. Do not force unsafe process conditions to create a failure. Where an actual condition cannot be reproduced safely, identify the limited simulation used and the portion of the chain it does not prove.
Handle untested conditions explicitly
A water test cannot establish performance in every production liquid. A static test cannot establish behaviour under severe agitation. Record such differences as open acceptance items with a responsible person and a defined follow-up condition. Depending on the consequence, the project may need a restricted operating range or a further witnessed trial before normal use.
Avoid a single pass/fail line for the entire installation. A project can pass its wiring check and steady-level comparison while still lacking evidence for the highest filling rate. Keep the separate results visible. This makes it possible to approve demonstrated functions without overstating the rest.
Independent overfill protection, where required, needs its own approved design and verification. A satisfactory inventory radar test does not establish safety integrity or make a second alarm derived from the same sensor independent.
Close the purchase with usable records
Before requesting a quote, provide the operating states to be demonstrated and say who will supply the reference, site access and test liquid. Ask whether commissioning attendance, diagnostic tools and configuration records are included. This lets the supplier price the required work rather than only the hardware.
Send the tank drawing and proposed acceptance schedule through the METRAVON enquiry page when assessing MV-RD14. Identify any condition that cannot be tested before production. Request a response to those particular conditions instead of a general statement that 80 GHz is suitable.
The handover should contain final settings, the actual installed dimensions, reference results, unresolved items and the reasons for any restrictions. Define review triggers such as a changed liquid, nozzle modification or revised control duty. A previous acceptance remains useful only while its assumptions still describe the installation.
Acceptance questions
Q1. Can a factory calibration report replace a site test?
No. It can support the instrument's performance under its stated test conditions, but it does not include the vessel nozzle, obstructions, process surface or control-system configuration. Use it as part of the evidence pack and verify the installed measurement separately.
Q2. What if a trustworthy high-level reference is unavailable?
Do not create a false pass from an estimated level. Agree a suitable reference method, a later controlled test or a clearly restricted acceptance. A successful low-level comparison alone does not prove high-level clearance or the required alarm response.
Q3. Should settings be changed until every test point agrees?
Investigate the pattern first. A consistent offset may indicate a datum error, while errors that vary with level or mixing can have different causes. Record each justified adjustment and repeat affected tests. Changing several settings at once can hide the original fault and invalidate earlier results.
Summary
Accept the installation against named operating states, a defensible reference and the required receiving-system behaviour. For MV-RD14, retain the exact configuration and geometry with the results. Separate actual measurement evidence from signal simulations, and leave untested production conditions visible until they are resolved.
