


 Chinese
 Spanish
 Russian
 Portuguese
 French
 German
 Indonesian
 Thai
 Vietnamese
 Arabic
 Italian
 Turkish
 Polish
 Japanese


Most plants still stamp a fixed calendar date on every level transmitter and call it a calibration plan. A flat annual interval either over-services stable instruments or under-services ones in harsh duty, because the interval is set by the diary rather than by how the device actually moves. A defensible interval comes from the observed zero drift of the fleet, recorded so it survives handover, and paired with a spares count sized to the failure rate and the supplier lead time.
Why a calendar date is the wrong interval
A calendar interval assumes every transmitter drifts at the same rate, which is false across a plant that mixes radar, ultrasonic and guided-wave devices in clean and coated services. A stable radar on a clean tank may hold its zero for years, while an ultrasonic above a steaming sump or a radar in a dusty silo can move within months. Servicing the stable one wastes a shutdown slot and risks introducing error during handling, and leaving the drifting one to a fixed date lets it exceed tolerance long before the date arrives. The interval should instead be the time for the observed drift to reach a chosen fraction of the acceptance tolerance, recomputed when the service or environment changes. This makes the plan defensible to an auditor who asks why a device was or was not opened.
Turning observed drift into a defensible interval
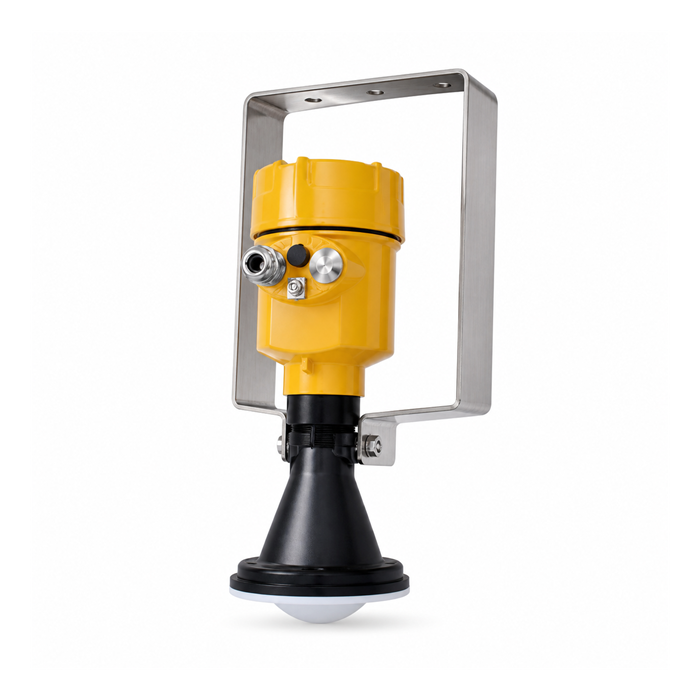
The interval follows from a simple ratio. Measure the zero drift over a known period, express it as a percentage of span, then divide the drift budget by the drift rate. As an illustrative calculation based on assumed site values: a transmitter shows 0.4 % of span drift over 6 months, an allowed tolerance of 1.0 % of span, and a chosen budget of half the tolerance (0.5 %) to leave margin. The other half is reserved for temperature drift and installation effects between calibrations. The drift rate is 0.4 % / 6 months = 0.0667 % per month. The interval is T = 0.5 % / 0.0667 % per month = 7.5 months, rounded down to a conservative 6-month plan. Input (0.4 % drift, 6 months) → conversion (rate then ratio) → result (6-month interval). Boundary: tighten the interval if the tolerance is stricter or the environment harsher, and recalibrate immediately on any single check that exceeds the 1.0 % tolerance regardless of the schedule, because drift rate is only an average.
A drift record sheet that survives handover
The value of a drift-based plan is lost if the underlying readings are not kept in a form the next technician can use. The record should capture identity, condition and result, not just a signed date, so a future reader can see whether the interval was earned or assumed. The fields below are the minimum a maintenance file should hold for each transmitter.
| Record field | What to enter | Why it matters |
|---|---|---|
| Tag number | unique loop identifier | links reading to the asset |
| Date and method | on-site dip vs reference | shows how zero was proven |
| Zero drift (% span) | signed value | feeds the interval formula |
| Process condition | temperature, coating noted | explains a change in rate |
| Next due date | computed interval | audit trail |
| Technician | name or initial | accountability |
A file built this way lets a new site owner continue the plan without re-deriving it, and it is the evidence an inspector expects during a management-system audit of the calibration programme.
Group sampling across a fleet
Calibrating every transmitter on a fixed date is expensive on a fleet of hundreds, so a sampled plan is common. Take a fleet of 120 transmitters and check a 10 % sample, or 12 units, each period. If all 12 stay within the 1.0 % tolerance, the interval for the group is confirmed or extended. One failure in twelve triggers a second 12-unit sample plus a check of the failed unit; two failures in the combined 24 recalibrate the group. The statistical strength grows with the sample size and the consequence of a miss, so a safety-related loop is sampled more heavily than a non-critical one. Input (fleet 120, sample 12) → conversion (pass or fail rule) → result (extend or tighten). Boundary: sampling only proves the untested majority by assumption, so the rule must escalate on the first failure rather than wait for the period to close, and critical loops should not rely on sampling at all where a hidden drift would breach a protection duty.
The confidence behind a sample follows from its size, not from the absence of failures. Twelve clean units leave the 95 % upper confidence limit on the defective fraction at about 22 % for zero failures in the sample, so such a sample can demonstrate a stable fleet but cannot prove a 2 % defect rate; roughly 150 clean units would be needed for that. Sizing the sample to the consequence means accepting that a passing group is evidence of stability, not a clean bill of health, and recording the confidence alongside the result so the next reviewer knows what the sample actually bought.
When a drift-based interval will mislead
Drift is a gradual, predictable movement, and an interval built on it says nothing about sudden failure. A lightning surge, water ingress through a damaged gland, a dropped antenna or a coating step-change on the process face are events, not drift, and they can take a transmitter out of tolerance between checks with no warning in the drift record. A new process temperature range or a change in the measured medium also resets the drift rate, so last year's interval may no longer apply. For these cases the plan must combine the drift interval with condition monitoring, such as echo-quality alarms and a zero-check on any maintenance visit, plus event-based recalibration after any fault or process change. Recalibrate on any visit where echo amplitude has fallen more than 6 dB below its commissioning value. A drift interval alone is a maintenance tool, not a substitute for protection-loop testing.
Spares quantity from failure rate and lead time
A spare-parts count sized to the fleet avoids both tying up capital in shelves of unused units and suffering long outages while a replacement ships. The quantity follows from the expected failures during the supplier lead time plus a small safety stock, computed per model family because failure rates differ by technology and duty. The table is an illustrative calculation based on assumed fleet data, to be confirmed against your own failure history and contract lead times.
| Model family | Fleet count | Annual failure rate | Lead time | Spares to hold |
|---|---|---|---|---|
| Radar 80 GHz | 60 | 2 % | 8 weeks | 2 |
| Radar 26 GHz | 30 | 3 % | 12 weeks | 2 |
| Ultrasonic | 20 | 5 % | 6 weeks | 2 |
| Gateway / RTU | 10 | 4 % | 10 weeks | 2 |
The calculation for the 80 GHz family is 60 × 0.02 × (8 / 52) = 0.18 expected failures in the lead time, rounded up and given one safety unit to hold 2. For the 26 GHz family, 30 × 0.03 × (12 / 52) = 0.21, also rounded to 1 + 1 safety. The small families follow the same rule rather than the raw number: 20 × 0.05 × (6 / 52) = 0.12 and 10 × 0.04 × (10 / 52) = 0.077 each round up to 1, and one safety unit brings both to 2. Longer lead times and higher rates, as in the 26 GHz family at 12 weeks, raise the hold even when the fleet is smaller. Boundary: hold at least one of every family present on site regardless of the math, because a zero-stock family with any failure stops a loop until the shipment arrives.
FAQ
Q1. Why not just calibrate every transmitter once a year?
Because drift rates differ by device and duty, a flat annual date over-services stable instruments and under-services drifting ones. A stable radar may hold zero for years while a coated ultrasonic drifts within months. An interval derived from observed drift targets the service where it is needed and is defensible to an auditor reviewing the plan.
Q2. How do I calculate the calibration interval from drift?
Measure zero drift as a percentage of span over a known period, find the rate, then divide your drift budget by that rate. In the worked example 0.4 % over 6 months at a 0.5 % budget gave a 7.5-month figure, rounded down to 6 months. Recalibrate at once if any single check exceeds the tolerance, since the rate is only an average.
Q3. Is sampling a fleet safe?
Sampling is safe for non-critical loops if the rule escalates on the first failure, with a second sample before any group-wide action, because an untested majority is only assumed good. Critical protection loops should not rely on sampling at all, and the sample size should grow with the consequence of a hidden drift breaching the duty.
Q4. What record proves the interval was earned?
A sheet with tag number, date and method, the signed zero drift in percent of span, the process condition, the computed next due date and the technician. This links each reading to the asset and lets a new owner continue the plan without re-deriving it, which is what an audit expects to see.
Q5. When does a drift interval give false confidence?
When the failure is an event rather than drift: surge damage, water ingress, a dropped antenna or a coating step-change are not predicted by the drift record. A new temperature range or medium also resets the rate. Combine the interval with echo-quality alarms, zero-checks on visits and event-based recalibration after any fault.
Q6. How many spares should I keep?
Size spares to expected failures during the lead time plus one safety unit, per model family. The worked table held 2 of an 80 GHz family and 2 of a short-lead ultrasonic family. Always keep at least one of every family on site, because zero stock on a family with any failure stops a loop until the shipment arrives.
SUMMARY
A calibration interval should follow observed drift, not the calendar: in the worked example 0.4 % of span drift over 6 months at a 0.5 % budget gave a 6-month plan, and the spares table held 2 units of a 60-device family against an 8-week lead time. Next, send us your fleet count by model, the tolerance you must hold and your supplier lead times, and our engineers will set the interval and the spares count for your sites.
Talk to a METRAVON engineer about this application
If you manage a fleet of level transmitters across several sites, send us the count by model, the tolerance each loop must hold and your supplier lead times. Our engineers will turn your drift records into a defensible calibration interval and a spares plan sized to your failure history.
