


 Chinese
 Spanish
 Russian
 Portuguese
 French
 German
 Indonesian
 Thai
 Vietnamese
 Arabic
 Italian
 Turkish
 Polish
 Japanese


Industrial weighing system selection for a skid or process vessel needs to account for the equipment after it reaches the plant. A factory test may be satisfactory while the installed weight drifts because pipework, access steel or transport restraints carry part of the load. Specify both the supplied measuring equipment and the site conditions under which its performance will be accepted.
Define the weighed assembly on the drawing
Mark the equipment that sits on the weighing supports: vessel, frame, motor, insulation, valves and any carried pipework. Then mark the items attached to the fixed plant. This separates true changes in supported mass from forces transmitted through external connections.
Decide whether the result is vessel inventory, a charge added to the vessel or material discharged from it. A before-and-after weight difference is useful only when the two readings represent comparable operating conditions. An agitator starting, a hose moving or a pipe heating between readings can affect the difference without representing material transfer.
Industrial weighing system selection: separate the delivery stages
| Stage | What can be checked | Checks still needed |
|---|---|---|
| Design review | Load cases, support positions, signal requirements and scope of supply | Actual installed performance cannot be inferred from a bill of materials. |
| Factory test | Assembly, wiring, calibration response and configured outputs | Effects of the permanent foundation and connected plant services still need site checks. |
| Site installation | Support condition, released transport restraints and final connections | Performance must be checked with the equipment in its intended measuring condition. |
| Process trial | Weight response during representative operating cycles | Untested recipes, temperatures or operating modes should not inherit an unrestricted acceptance. |
Write these stages into the purchase specification. A factory acceptance test and a site acceptance test should have distinct records and responsibilities. State who provides reference loads, safe access, installation labor and the process material for trials. Otherwise, a quotation can appear complete while excluding the work needed to put the scale into service.
Match component capacity to the required net measurement
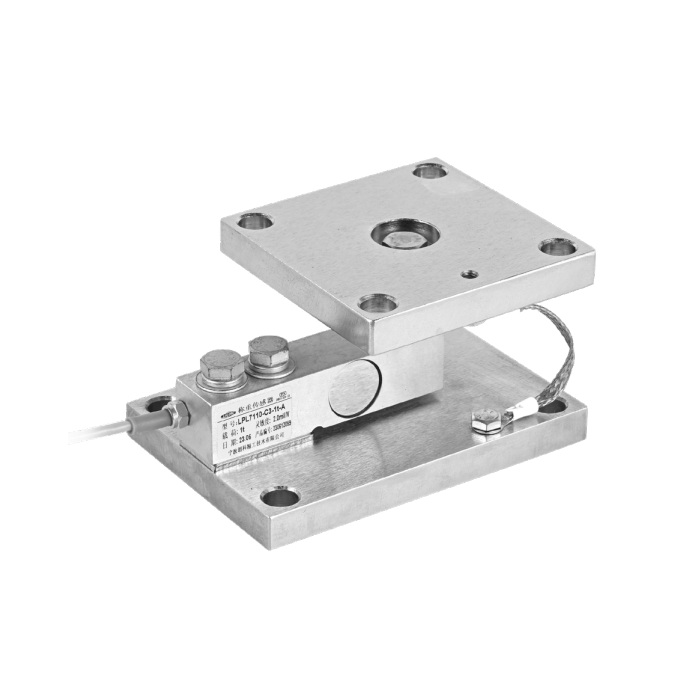
METRAVON MV-WM0006 has published capacity groups of 0.5-2.5 t and 3-5 t. These are module selections, not total skid capacities. The maximum reaction at each support and the assembly drawing determine whether a particular version is suitable.
Do not use the sum of nominal support capacities as the only calculation. An offset center of gravity, pipe restraint or uneven foundation can place more load on one support. The tank support-load guide addresses those mechanical checks; the module installation guide covers height and service access.
Check the smallest required net change separately from gross capacity. For example, a hypothetical skid carrying 2,000 kg of equipment may need to distinguish a 1 kg addition. Those example masses do not establish a suitable model or achievable accuracy. They illustrate why the minimum addition, signal noise and installed repeatability must be evaluated together. Taring the equipment does not recover mechanical capacity or increase the electrical signal produced by that addition.
Make the controls contract explicit
Identify the device that calculates weight and the system that acts on it. A PLC, HMI and data logger can display different values if units, tare or filtering are applied at multiple points. Assign gross weight, net weight and tare clear meanings and verify those meanings at each destination.
Request the actual interface details of the selected instrument, not simply a requirement for RS485. If Modbus RTU is proposed, obtain its register map and supported data representation. For an analog input, specify the current range, weight endpoints and response to an invalid signal. The load-cell signal-chain article provides the detailed electrical checks.
Review startup, power recovery and maintenance behavior. A stored tare may be appropriate for one operation and misleading for another. Test that a disconnected or stale signal is identified rather than silently accepted as a valid weight. Do not assume measurement fault handling provides a safety-rated shutdown.
Accept the site result and preserve the useful records
Inspect the final load path before calibration. Compare zero return and repeated applied loads, then check the value received by the control system. Exercise normal valve, pump and mixer states where relevant, and investigate weight shifts before compensating them with software.
For transfer or batching duties, follow calibration with a material trial that represents the required operation. Agree tolerances and test conditions in advance. Retain support-position identification, final drawings, settings and measured results so later piping or software changes can be compared with the accepted installation.
Questions for a skid weighing project
Q1. Can factory calibration be accepted without site testing?
Only if the acceptance arrangement justifies it for the supplied and installed conditions. Transport, foundations and permanent connections can change the load path. For a skid connected to plant pipework, include checks after those connections are completed instead of treating factory calibration as proof of site performance.
Q2. Should the purchase include only modules or a complete system?
That depends on who will supply the electronics and perform integration. Either scope can work when the responsibilities are stated. List modules, junction box, indicator or transmitter, cables, calibration and commissioning separately so comparable quotations include comparable work.
Q3. What should be sent with an enquiry?
Provide the skid drawing, supported equipment list, maximum contents, smallest required weight change, operating sequence and site interface requirements. Identify any work already assigned to the plant integrator. Use the METRAVON enquiry page to request a component or system quotation against that defined scope.
Summary
For plant and skid weighing, specify what will be weighed and how performance will be checked after installation. Component selection, factory testing and site acceptance answer different questions. Keeping them separate prevents an incomplete equipment quotation from being mistaken for an accepted process measurement.
