


 Chinese
 Spanish
 Russian
 Portuguese
 French
 German
 Indonesian
 Thai
 Vietnamese
 Arabic
 Italian
 Turkish
 Polish
 Japanese

Grain and feed silo monitoring needs to distinguish material in storage from material available to the next process. A high surface reading does not prove that a hopper outlet is feeding, and a successful delivery does not prove that the material reached the intended silo. METRAVON radar, point-level and weighing products can support these checks when each signal is assigned a clear task in the receiving, storage and batching sequence.
Start with the material route through the plant
Identify the destination silo, inlet route, outlet feeder and downstream equipment for each material. Record where an operator selects a route and where the control system confirms it. Level information is useful only when the silo identity and material identity are correct; an accurate reading attached to the wrong tag can lead to an incorrect delivery decision.
Separate storage duties from recipe duties. Radar can help show remaining capacity and stock trends. A point switch can indicate material at a chosen location. A weighing stage can check a delivered batch quantity. None of these measurements, by itself, confirms grain quality, moisture, temperature or freedom from contamination.
Grain and feed silo monitoring duties
| Duty | Signal to use | What it does not establish |
|---|---|---|
| Delivery planning | A validated level or inventory value, with a current timestamp and known silo identity. | Enough safe filling capacity without allowing for the actual pile shape, transport delay and stopping sequence. |
| High-level alarm | A defined continuous alarm or separately assessed point detector and shutdown path. | Independent protection simply because the same sensor value appears on two displays. |
| Feed continuity | Feeder command and feedback, downstream response, and suitable material-presence information. | Free flow at the outlet merely because material is visible higher in the silo. |
| Recipe dosing | An accepted weight for each required addition, associated with the recipe and material. | Correct ingredient proportions from total batch weight alone. |
| Stock reporting | Time-aligned measurements and receipt/withdrawal records with their conversion assumptions. | A direct mass measurement when tonnes were calculated from level and a fixed density. |
Use radar to follow the surface, not to diagnose every blockage
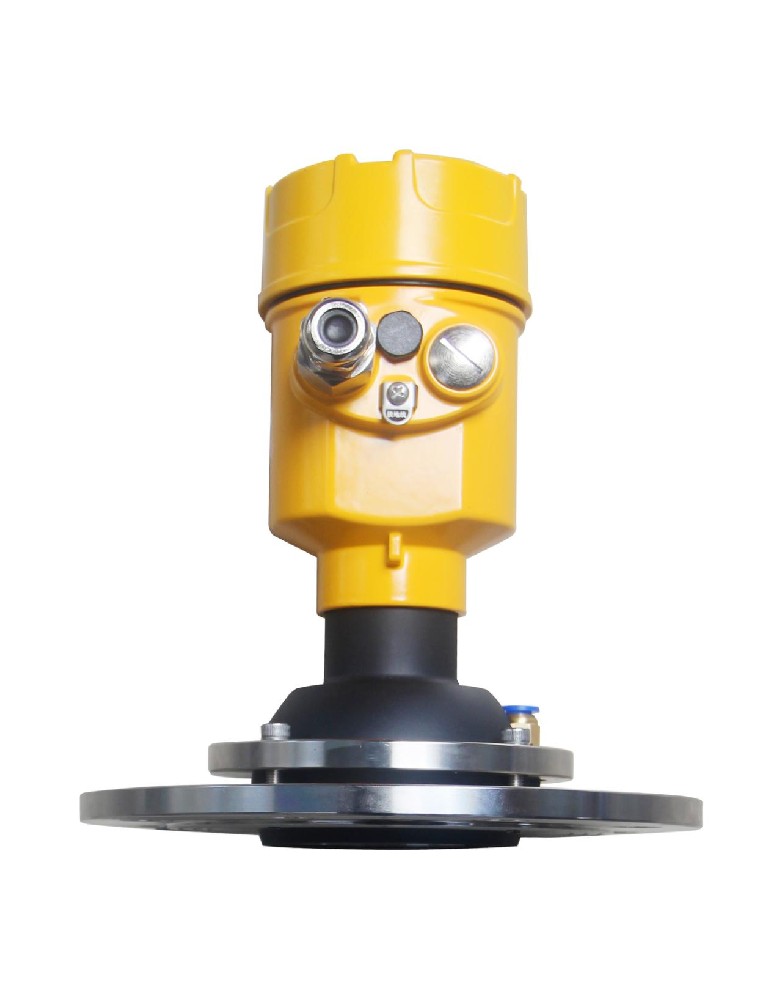
The MV-RD21S has a PE-lens configuration for bulk solids and a documented process-temperature reference up to 80 deg C. This is not a general approval for hot dryer discharge or every dusty environment. Include the temperature at the antenna, dust behaviour, potential deposits and any required hazardous-area documentation in the selection review.
Choose the roof position with the inlet stream and expected pile profile in view. Avoid direct material impact, nearby roof steel and an installation that looks at a wall instead of the changing surface. Check the response during filling as well as after the material has settled. A good empty-bin echo is only one part of commissioning.
Bridging and ratholing can leave material high in the vessel while restricting discharge. If the feeder is commanded on but the downstream process receives no material, compare equipment feedback and local process indications. A radar surface trend alone cannot identify the exact mechanical cause or prove that an outlet is clear.
Position and test the point-level alarm
The MV-SP601 can be assessed for a defined high or low material-presence check. Select the rod or cable arrangement from the mounting position, active sensing region and material forces. A cable must not be placed where normal flow or moving equipment can load it beyond its approved installation conditions.
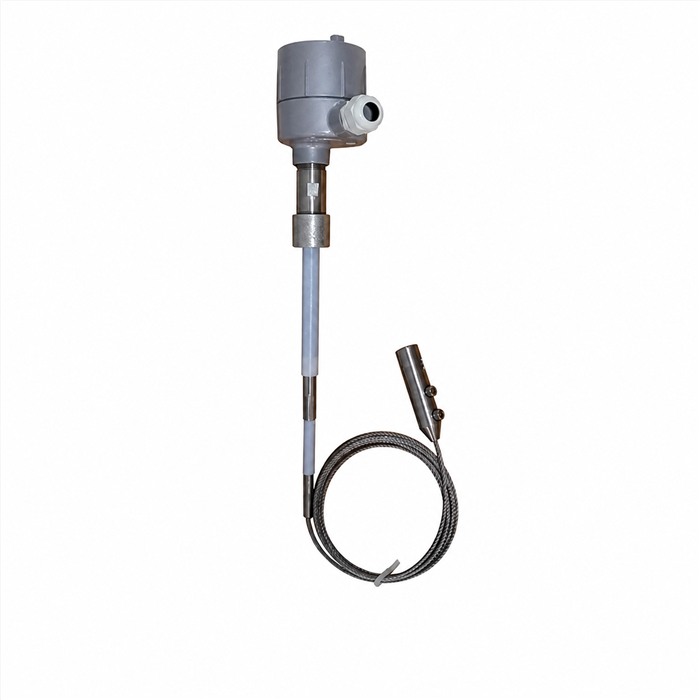
Choose a high-level trigger with the filling shutdown sequence in mind. Material can remain in a conveyor, spout or pneumatic line after the upstream feed is stopped. The required free space depends on that residual delivery and the delay in the selected controls. Determine it for the installation instead of applying an arbitrary alarm percentage to every silo.
Test material present and absent, then check whether normal residue prevents the sensor from returning to its clear state. Confirm the alarm at the control input and the intended equipment response. A simulated input can prove the logic downstream but does not demonstrate that the probe detects the actual grain or feed.
Keep batching evidence separate from storage estimates
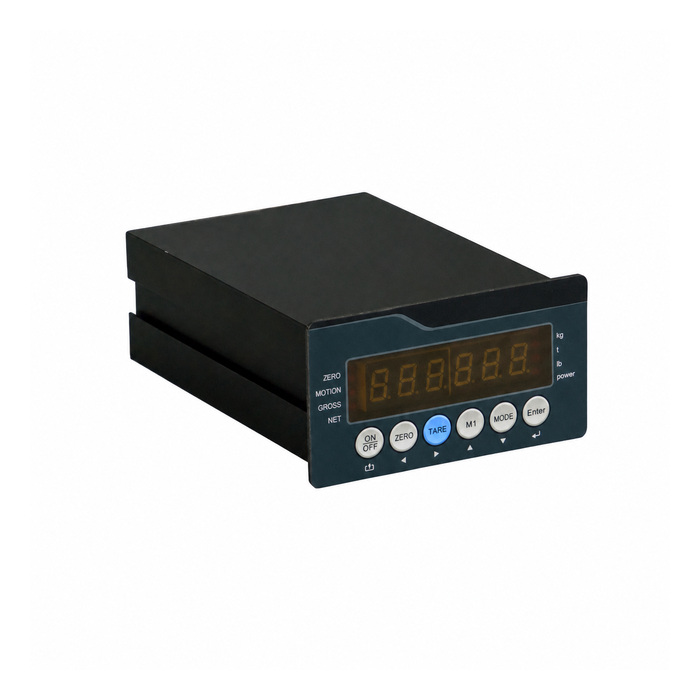
At the dosing stage, the MV-WI0009 weighing controller provides an option for indication, relay I/O and selected communications. Its four relay outputs are not evidence of an unlimited recipe program. Establish the number of feed stages, interlocks and stored recipes required, then allocate them between the controller, PLC and supervisory software.
Test minor additions as well as the largest batch. Feeder flow can vary with ingredient properties and supply level, while material already falling continues to arrive after a cutoff command. The accepted record should contain the actual ingredient additions, not only the final total. See the batch weighing guide for trials and control allocation.
Commission with the operating conditions that cause trouble
Plan checks for dusty filling, normal discharge, low stock, a change of material and recovery after a power or communication interruption. Save the raw level, converted inventory, material identifier and equipment states. Compare these time-aligned records before deciding that a stock discrepancy requires sensor adjustment.
For inventory estimates, document the density and surface assumptions used for each stored product. Moisture and settling can change the conversion from occupied volume to mass. A single density value reused across different grains or feed blends can create systematic purchasing errors even with repeatable level readings.
Inspection access and fault response must account for grain-handling hazards. Do not enter onto or beneath bridged grain to verify an instrument or restore flow. Use the site's isolation, access and rescue procedures with qualified personnel. A level alarm is not permission to enter a bin, and a generic instrument enclosure rating is not proof of suitability for a combustible-dust location.
Questions from plant and maintenance teams
Q1. Why does a silo show stock when the feeder has run empty?
Stored quantity and outlet availability are different. Bridging, a blocked outlet, the wrong gate position or a failed feeder can interrupt flow while material remains. Check equipment states and process observations safely before changing the level scale.
Q2. Can one instrument handle inventory and the high-level stop?
It may provide both an operating value and an alarm, but their common failure modes remain. Decide whether a separate detector and control path are required from the process risk assessment. The number of configured alarms does not establish independence.
Q3. Does the radar measure grain moisture or temperature?
No such function should be inferred from level measurement. Those duties need suitable separate measurements and an appropriate monitoring plan. Moisture information may improve the interpretation of a density-based stock estimate, but it is not generated by the level reading itself.
Q4. What should be included in an enquiry?
Provide materials, silo and hopper drawings, inlet and outlet arrangements, temperatures, dust conditions and the available electrical interfaces. Identify each required alarm action, recipe tolerance and reporting task. Include the site's hazardous-area requirements and access constraints so unsupported safety or maintenance assumptions do not enter the quotation.
Summary
Reliable grain and feed monitoring assigns a separate purpose to surface measurement, material-presence alarms and batch weighing. Preserve material identity and measurement validity throughout the system, then verify the real receiving and discharge sequences. Share the plant material routes and measurement duties with METRAVON for a product-specific review.
