


 Chinese
 Spanish
 Russian
 Portuguese
 French
 German
 Indonesian
 Thai
 Vietnamese
 Arabic
 Italian
 Turkish
 Polish
 Japanese


An industrial weighing system needs one agreed acceptance result at the point where weight is used. A load cell certificate, a calibrated transmitter and a PLC display can each look satisfactory while inconsistent tare or scaling produces the wrong batch quantity. Assign responsibilities before the mechanical and controls packages are ordered separately.
Industrial Weighing System: Divide the Supply Scope Clearly
| Package | Supplier deliverable | Handover evidence |
|---|---|---|
| Mechanics | Support reactions, mounting drawings and restraint arrangement. | As-built load path and inspection access. |
| Measurement | Cells, excitation, junction arrangement and calibrated input range. | Sensor identities, wiring and reference-load results. |
| Controls | Units, tare ownership, filtering and fault response. | PLC readings and sequence behaviour using the installed equipment. |
| Verification | Reference method, test points and permissible deviations. | Signed results with configuration and process state. |
Name the party responsible for discrepancies between packages. Without that agreement, a mechanical installer may accept the unloaded structure while the controls team calibrates around pipe forces introduced afterward.
Freeze the Gross-Load Design Before Setting Net Weight
Record the vessel or platform dead load, maximum contents and the highest reaction at an individual support. Include equipment added after the initial survey. Define which movements the support assembly permits and which forces are carried by separate restraints.
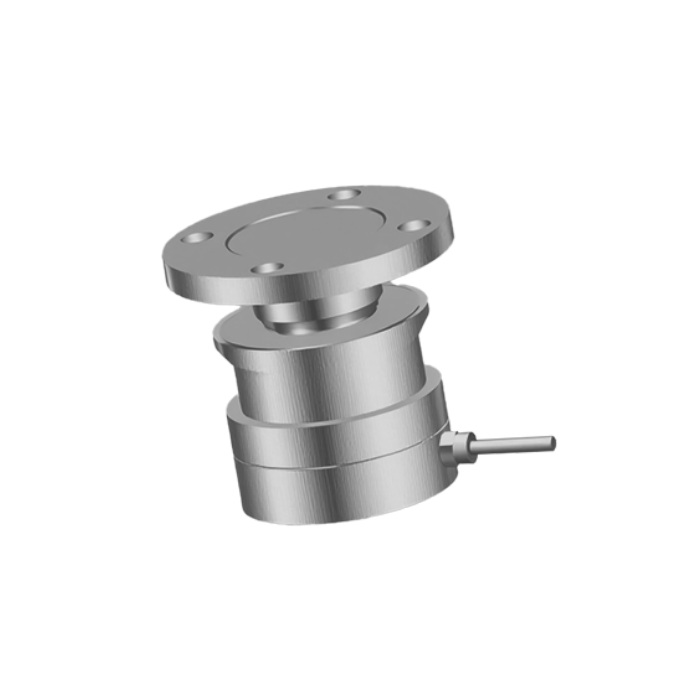
The MV-WM0007 uses a cylindrical compression arrangement. Its capacity-dependent flange dimensions do not establish a digital output, a complete anti-uplift system or the accuracy of the assembled vessel. Confirm each of those requirements separately.
Use a Shared Configuration Record
Record the physical load assigned to zero and span, the engineering unit, the device applying tare and the meaning of each reported status. Prevent an HMI recipe from applying another tare to an already net-weight value. Back up settings outside the instrument and record who may change them.
For batch control, test the response from physical loading through the cutoff action. Filtering that makes inventory readings easier to read can delay a stop decision. Test representative transfer rates; do not infer dynamic performance from a settled reference weight.
Acceptance Sequence
- Inspect the final connected structure and remove temporary supports according to the installation procedure.
- Record individual support information where the hardware allows it, then verify zero, loading, unloading and repeatability.
- Compare the local weight, transmitted value and PLC interpretation at the same load.
- Exercise the documented fault and restart responses without creating an uncontrolled process condition.
Q1. Can commissioning finish before the pipework is connected?
That can establish an intermediate baseline, not final installed acceptance. Repeat the relevant checks after services, guards and access equipment are in their operating positions.
Q2. Must every system expose individual cell diagnostics?
No. That capability depends on the electronics and wiring. Specify the required diagnostic access in the quotation; an analog summing box does not automatically provide separate digital channels.
Summary
Purchase an agreed mechanical, measurement and controls scope with one acceptance plan. Send the package responsibilities and process sequence for an industrial weighing system review, including any existing equipment that must remain.
