


 Chinese
 Spanish
 Russian
 Portuguese
 French
 German
 Indonesian
 Thai
 Vietnamese
 Arabic
 Italian
 Turkish
 Polish
 Japanese


A hopper weighing system must be specified around what the process needs to measure: material entering a receiving hopper, material leaving a feeder, or stock remaining between transfers. Those quantities are related, but they are not interchangeable. The control sequence and the point where material is considered delivered should be defined before selecting the weighing hardware.
Receiving a batch and controlling a feeder are different duties
| Duty | Measured quantity | Main verification question |
|---|---|---|
| Gain-in-weight | Increase in receiving-hopper weight | Does the settled received amount meet the batch requirement after cutoff and material in flight? |
| Loss-in-weight | Decrease in feeder-system weight over time | Does the measured loss represent outlet delivery during normal feeding, and how is refill handled? |
| Inventory | Material remaining at a defined reading condition | Can the reading be compared consistently despite buildup, connected services and operating state? |
In a receiving batch, material can still be falling after the inlet device is commanded to close. In a loss-in-weight feeder, the rate calculation uses a change in weight over time. Selecting one filter setting for both duties without a process trial can produce either unstable rate estimates or a delayed batch cutoff.
Select a hopper weighing system for the smallest useful quantity
List the empty hopper, feeder, motor, gate and any equipment carried on the weighing supports, then add the maximum contents and relevant operating loads. Electronic tare subtracts an indicated value; it does not remove the mechanical load from the cells.
Next identify the smallest ingredient addition, batch or rate change that matters. A small addition to a heavily loaded hopper uses only a small portion of the system's gross range. Verify the signal change, noise and repeatability at that operating point rather than relying on the number of displayed decimal places.
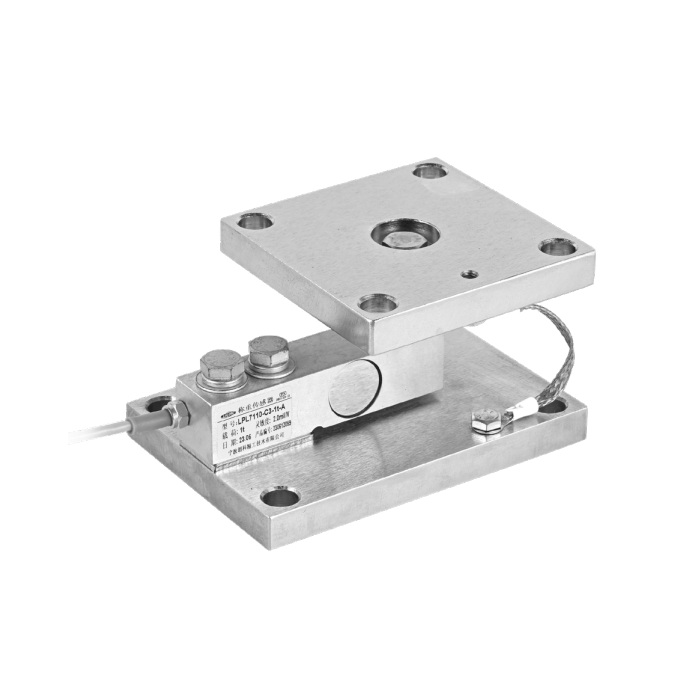
METRAVON MV-WM0006 is a module option to review where its capacity group and mounting arrangement suit the support design. Its published groups are 0.5-2.5 t and 3-5 t, with different assembly heights. That information does not establish feeder throughput, batch accuracy, hygienic suitability or controller functions. Small dosing equipment may require a different mechanical and capacity arrangement.
For support dimensions and retrofit checks, refer to the module installation guide. The hopper drawing should identify the weighed assembly clearly so the purchaser and integrator agree which motors, gates and connections are included in the measured mass.
Account for refill, flow aids and retained material
During refill of a loss-in-weight feeder, the weight change contains both incoming material and outgoing feed. It cannot directly represent outlet flow from weight loss alone. Ask the selected controller supplier how feeding is controlled during this interval, how the interval is flagged and when valid gravimetric control resumes. Do not assume those capabilities are supplied with the module.
Bridging, aeration and changes in bulk density can alter feeding behavior even when the static scale remains correct. Test the actual powder, granules or other material at representative conditions. Record the use of agitators and vibrators, since their operation can affect both material flow and the force signal.
Distinguish material leaving the weighed assembly from material reaching its destination. Product retained in a fixed discharge chute, leakage or diversion after the hopper outlet can cause a difference. Define the receiving point for a delivery test and ensure the reference collection captures the intended output safely.
Remove external forces before tuning the controls
Inspect inlet sleeves, outlet connections, extraction ducts, air hoses and electrical conduits. A nominally flexible connection can still transmit vertical force when stretched, packed with material or displaced. Check it across the normal fill level and operating movement, not just with the empty hopper stopped.
Pressure changes can also act on the weighed assembly through connected equipment. If the weight shifts when extraction or a valve operates, investigate that physical effect before increasing filtering. Filtering can smooth the displayed change while leaving its bias and the resulting dosing error unresolved.
Separate scale calibration from material acceptance
First verify the static measuring chain using an agreed reference method. Then run material trials covering the intended small and large batches or feed rates, relevant hopper levels, startup and refill recovery. Define tolerances and the number of runs in the test plan; no universal percentage or run count is appropriate for every material and process.
For receiving batches, compare the settled batch result with an independent reference where practicable and record cutoff behavior. For loss-in-weight duty, a controlled collection test over a measured interval can check delivered mass and average rate. Reference weighing uncertainty, collection losses and timing uncertainty must be suitable for the claimed result.
Keep each trial's recipe, fill level, material condition, filter settings, feeder command and refill state with its result. This makes an error traceable to a physical or control condition instead of encouraging repeated changes to an unexplained correction factor.
Questions about hopper performance
Q1. Why is a small ingredient inaccurate when the total batch looks correct?
The ingredient increment may be too small relative to the gross range and measurement noise, or the inlet device may have poor cutoff control at that quantity. Test that ingredient independently at the actual hopper loading condition before changing the full-scale calibration.
Q2. Can longer averaging solve an unstable feed-rate display?
It can reduce visible variation but adds delay and may conceal intermittent flow. Check mechanical disturbance and material flow first, then evaluate the controller response with the proposed averaging. The accepted setting must work during normal feeding and recovery from refill.
Q3. What information is needed for a quotation?
Provide the hopper and support drawing, empty and maximum loaded weight, material description, minimum batch or feed-rate requirement, control sequence and destination interface. Identify whether the request covers modules only or also instruments and integration. Submit those details through the METRAVON enquiry form; the price depends on that defined scope.
Q4. Does passing calibration prove material delivery is correct?
No. Calibration checks the weighing response under its test conditions. Actual delivery also depends on flow, cutoff, retained material and refill behavior. Accept the installation only after the relevant material-transfer tests meet the separately agreed process limits.
Summary
Define the measured quantity, smallest useful increment and refill behavior before selecting hopper weighing hardware. Verify the static scale and the material-transfer process separately. This keeps a mechanically suitable module from being mistaken for a complete, proven dosing system.
