


 Chinese
 Spanish
 Russian
 Portuguese
 French
 German
 Indonesian
 Thai
 Vietnamese
 Arabic
 Italian
 Turkish
 Polish
 Japanese


A conveyor load cell does not need a large fault to produce a large daily stock discrepancy. If a belt scale retains a small positive load per metre while the empty belt runs, the totalizer integrates that bias for the entire running period. Replacing the sensor without examining the empty-running trend may leave the same error in place.
How conveyor load cell zero bias becomes accumulated mass
For an illustrative belt-scale calculation, assume the false load is 0.2 kg/m and belt speed is 2 m/s. Their product is 0.4 kg/s, equivalent to 1.44 tonnes in one hour. This is a calculation example, not measured performance of a METRAVON product. The actual error depends on the bias and the time for which the integrator counts it.
Read the load signal, speed signal and total together. A total that changes while the displayed rate is rounded to zero may reflect hidden resolution, filtering or totalizer logic. Record the unrounded values available from the instrument before deciding which device is responsible.
| Pattern | Look for | Next check |
|---|---|---|
| Steady bias | Similar empty-belt load throughout a full revolution | Zero procedure, retained material and mechanical restraint |
| Once per lap | A feature repeating with the belt splice or a marked position | Belt variation and carriage response over complete revolutions |
| Speed linked | Bias changing when belt speed changes | Dynamic belt forces, alignment and speed measurement |
| Only totals | Rate looks correct but accumulated mass does not | Integration units, counting conditions and low-flow settings |
Use an empty-running test without hiding light material
Remove residual material using the site's isolation and cleaning procedure. Inspect the carriage for contact with guards, packed deposits or tight cable restraints. Run the empty belt through complete revolutions under the conditions required by the scale manufacturer; a stationary zero does not capture belt-induced forces.
A zero-tracking or low-flow cutoff setting can suppress accumulation, but it can also discard genuine light loading. Record the existing settings before altering them and repeat a controlled material test afterward. The useful result is correct empty and loaded behaviour, not simply a totalizer that stays still.
Where the sensor specification matters
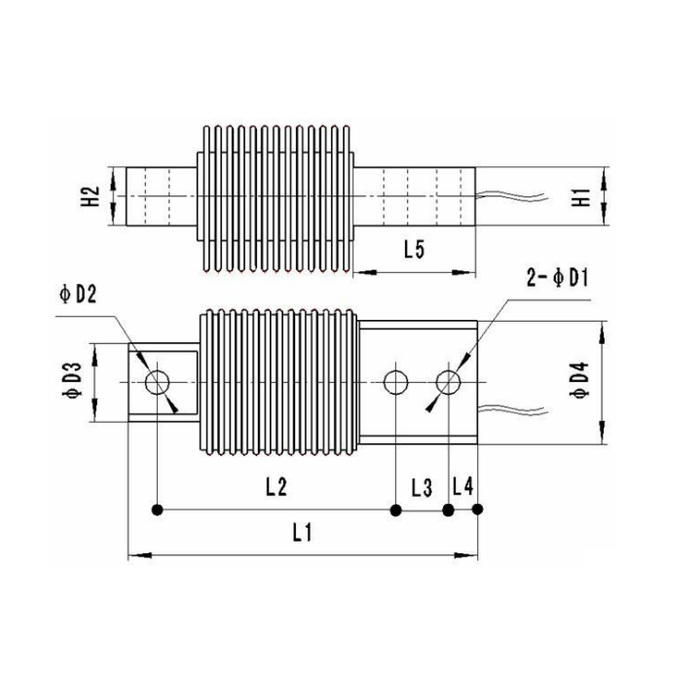
METRAVON MV-LC0065 is listed at 10-500 kg with 2.0 +/-0.01 mV/V output and 10-12 VDC excitation. These values describe the load cell, not the accuracy of a complete conveyor scale. The carriage design, belt forces, speed pickup and integrator remain part of the measurement. Confirm installation dimensions before proposing it for an existing frame.
Questions about unexplained totals
Q1. Will a new zero calibration fix a repeating spike?
It may change the average, but it will not remove a mechanical disturbance tied to one belt position. Identify the repeating feature and compare several revolutions before accepting a new zero.
Q2. What should accompany a replacement enquiry?
Include an empty-running trend covering complete belt revolutions, speed, total change, old sensor data and carriage photographs. These distinguish a sensor request from a belt-scale diagnostic problem.
Summary
Quantify how much false mass is accumulating and when it occurs. Send the empty-belt record to METRAVON with the mounting drawing so sensor compatibility can be reviewed without treating a cell replacement as a guaranteed cure for totalizer error.
