


 Chinese
 Spanish
 Russian
 Portuguese
 French
 German
 Indonesian
 Thai
 Vietnamese
 Arabic
 Italian
 Turkish
 Polish
 Japanese


A batching plant load cell measures the supported load, not the dry aggregate content or the water available to the mix. A correctly calibrated scale can therefore deliver the requested wet mass while the recipe receives the wrong dry-solids amount. Keep the weighing measurement and moisture correction as separate, traceable operations.
Define the Moisture Basis Before Using a Percentage
For an explicit dry-basis example, suppose water mass is 5% of dry aggregate mass. A target of 1000 kg dry aggregate then corresponds to 1050 kg wet material: 1000 kg solids plus 50 kg water. This is an illustrative mass balance, not a recommended recipe or a moisture-sensor specification.
A percentage expressed on a wet-mass basis gives a different conversion. If water were instead 5% of the total wet mass, 1000 kg of dry solids would require 1000 divided by 0.95, or approximately 1052.63 kg wet mass. The two examples use different percentage definitions; neither establishes the free-water correction for a concrete recipe. The plant's recipe also needs its approved treatment of absorption and free moisture; not all measured water should automatically be subtracted from the batch-water setting. Identify the convention used by the laboratory, controller and operator display before enabling correction.
| Quantity | Origin | Must not mean |
|---|---|---|
| Wet mass | Installed weighing system after tare correction. | Dry aggregate mass without a moisture calculation. |
| Moisture | Representative sampling or an approved measurement method. | A permanent property shared by every stockpile and delivery. |
| Recipe mass | Controlled mix design and documented correction logic. | A raw load-cell output or an arbitrary scale offset. |
Batching Plant Load Cell Selection Still Depends on the Structure
MV-LC0150 is a single-ended shear beam with capacity-specific mounting dimensions and an analogue bridge output. It is a candidate component only where the hopper support design suits that load path. Include hopper tare, uneven support loading and filling impact; dividing total contents by the support count is not a complete selection calculation.
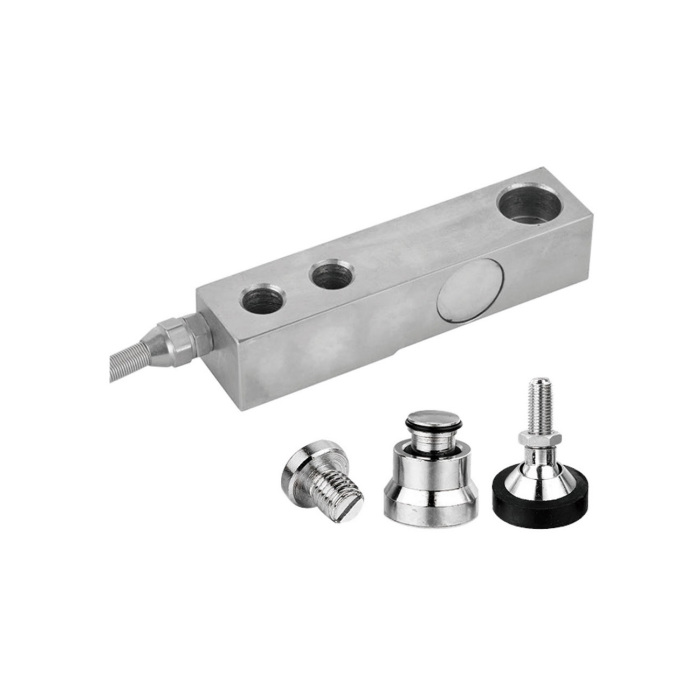
The indicator or weighing transmitter converts the bridge signal into a usable weight. Recipe software then applies the approved moisture calculation. Do not alter the scale calibration to force agreement with a recipe that uses outdated moisture data; that creates an error in every subsequent weight measurement.
Test a Batch With Both Records Visible
Retain the uncorrected weight, moisture input, corrected target and final discharge result for the same batch. Confirm that changes to moisture affect the intended calculation only. Independently verify scale performance with the accepted reference method, and check residual material if delivered quantity differs from hopper loss.
Plant Operation Questions
Q1. Does a more accurate cell fix variable moisture?
No. Better force measurement cannot identify how much of the measured mass is water. The moisture input must represent the material entering the weigh hopper and use the recipe's defined basis.
Q2. What should the load-cell enquiry include?
Send the hopper drawing, support reactions, gross load, feed sequence and existing weighing electronics. Identify the required weighing performance separately from moisture-correction and recipe-control responsibilities.
Summary
Use MV-LC0150 only after the mechanical and electrical fit is established. Preserve an independently verified weight signal, then apply the documented recipe correction without disguising process variability as a scale-calibration problem.
