


 Chinese
 Spanish
 Russian
 Portuguese
 French
 German
 Indonesian
 Thai
 Vietnamese
 Arabic
 Italian
 Turkish
 Polish
 Japanese

Food ingredient weighing has two acceptance questions: was the required quantity delivered, and can the equipment be released for the next production run under the plant's cleaning procedure? A weigh module can address the first question only as part of a complete hopper assembly. Its material or enclosure description does not establish hygienic suitability, allergen removal or approval for food contact.
Decide what must be cleaned before choosing the weighing hardware
Identify the hopper's product-contact surfaces, discharge gate, flexible sleeves and transfer path. Then identify components outside that zone that can still be exposed to dust, condensate or washdown. The weighing supports may sit outside the product path, but their location can affect access, drainage and the ability to inspect the hopper underside.
Specify dry cleaning, wet cleaning or a combination, including the chemical, temperature and exposure method. A stainless component is not automatically suitable for every cleaner, and an ingress rating alone is not a statement about high-pressure washing or chemical resistance. Obtain the requirements for the selected assembly instead of extending a sensor label to the entire machine.
| Area | Question to resolve | Evidence for release |
|---|---|---|
| Hopper | Can product-contact surfaces and the outlet be inspected and cleaned as required? | Approved fabrication details and the plant's demonstrated cleaning procedure. |
| Sleeves | Does the connection retain residue or exert force on the weigh vessel? | Inspection access plus weight checks in the final connected condition. |
| Supports | Can dust or cleaning fluid accumulate around the modules and restraints? | Suitable layout, environmental specification and inspection access. |
| Batch data | Are ingredient identity, accepted mass and exceptions linked to the batch? | A retrievable record for normal, rejected and interrupted production. |
| Changeover | Who authorises the next product after cleaning and clearance? | The defined release record, not a zero reading used as a substitute. |
Food ingredient weighing starts with the loaded assembly
The METRAVON MV-WM0022 is a bellows weigh module for small vessels. Consider it as a weighing component beneath a suitably designed hopper, not as a complete hygienic dosing machine. Ask for the proposed module materials, environmental limits and mounting dimensions to be checked against the installation and cleaning exposure.
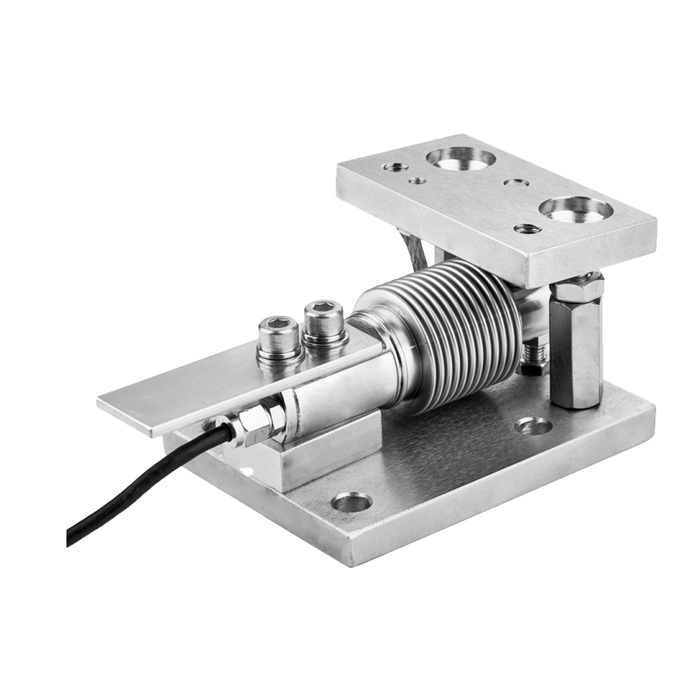
Include the empty vessel, gate, agitator or feeder attachment and maximum ingredient quantity in the support-load assessment. Uneven loading and actuator forces can make the largest support reaction greater than a simple equal division of total mass. The smallest recipe addition also matters: it must produce a measurable change under real production disturbances.
Check the empty indication with the inlet and outlet sleeves in their final positions. Repeat while valves operate and extraction or conveying equipment runs. A connection that pulls on the hopper can create an apparent quantity change without any ingredient entering it. Resolve that force path before compensating it with tare or software.
Accept the ingredient addition, not just a plausible total
Set an allowed error for each ingredient where the recipe requires it. A correct final batch weight can hide an excess of one ingredient and a shortage of another. For a small addition on top of a large accumulated load, demonstrate the result at that stage of the recipe rather than testing only an empty hopper.
Separate the accepted quantity in the weigh hopper from the quantity reaching the mixer. Sticky ingredients or fine powders can remain at a gate or in the transfer line. If the process relies on complete discharge, define how retained material is detected and what happens to an incomplete transfer. Automatic zeroing should not erase the evidence needed to make that decision.
Test start and stop behaviour using representative ingredients. Record feeder cutoff, settled result, discharge residue and cycle time. Establish tolerances from the production specification; there is no universal error figure that makes a dosing system acceptable for every ingredient or recipe.
Give the weighing instrument a defined role in the batch record
The MV-WI0009 provides weight indication and configurable I/O options for an agreed control scheme. A PLC or supervisory system may still be responsible for recipe versions, ingredient lots, operator permissions and historical records. Confirm that allocation before assuming the instrument alone provides batch traceability.
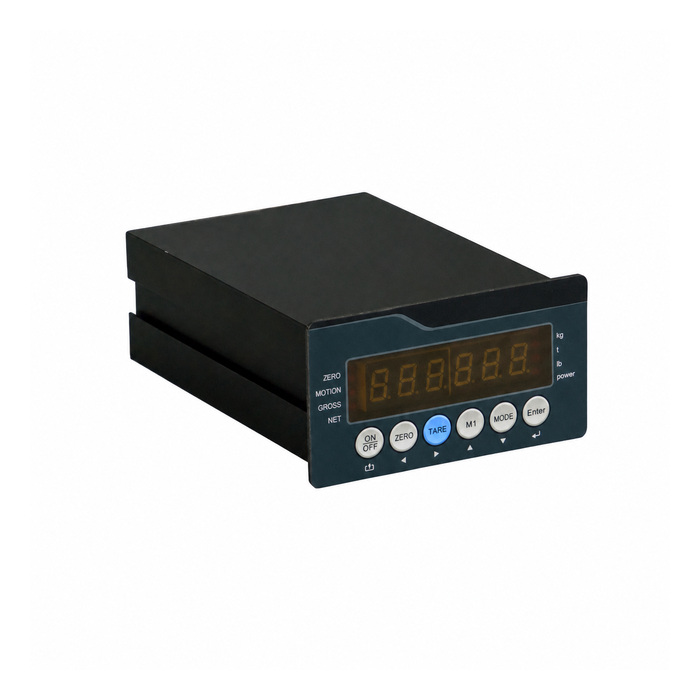
Where Modbus RTU or 4-20 mA is needed, identify the option in the order and verify its wiring and data definition. For digital acquisition, distinguish live weight, stable accepted weight and an invalid or interrupted result. A saved number without its status cannot reliably explain what happened during production.
Agree the behaviour after a power failure or aborted recipe. The operator may need to identify and dispose of a partial batch before restart. Do not let a restored communication link turn an unfinished addition into an apparently completed record.
Prove changeover separately from weighing accuracy
Following cleaning and reassembly, inspect the defined areas and complete the plant's release procedure. Then verify that sleeves, restraints, cables and supports have returned to their approved positions. An accurate pre-cleaning calibration does not reveal a hose reconnected under tension afterwards.
Keep the cleaning record separate from the weighing check while linking both to the equipment identity. A zero indication can coexist with retained material if tare has been applied. It is therefore not evidence of allergen removal or absence of residue. The site's responsible food-safety team must define and verify those criteria.
Questions about a new dosing installation
Q1. Can an ordinary weigh module be described as food-grade?
Not without a defined claim and supporting documentation. State whether the module contacts product and which material, cleaning and environmental requirements apply. Evaluate the complete hopper installation rather than using food-grade as a general label for weighing accuracy or stainless construction.
Q2. Can silo level replace ingredient weighing?
Level is useful for replenishment and stock trends, but a recipe quantity may require a directly verified mass. Uneven surfaces, density changes and silo geometry complicate conversion. The inventory measurement comparison helps separate those duties.
Q3. Why does the zero move after washing?
Check retained liquid, sleeve position, restraint contact, cable forces and moisture exposure before recalibrating. Record whether the change disappears after drying or after a mechanical connection is corrected. Repeated tare adjustments can conceal the underlying problem.
Q4. What documents should accompany the enquiry?
Include the recipe range, smallest addition, hopper and support drawings, cleaning specification and required material documents. State the batch-record fields and release responsibilities. Ask the quotation to distinguish weighing hardware from vessel fabrication and control software.
Summary
Food ingredient weighing requires verifiable quantities without losing sight of cleaning and changeover. Discuss the hopper and measurement requirements with METRAVON, while keeping hygienic approval and food-safety release tied to the complete equipment and the plant's documented procedure.
